Explore our export-grade multi-axis oxyfuel torch systems, cold-cutting pipe split frames, and automated plate edge milling solutions built for heavy structural steelwork.








A comprehensive technical evaluation of flame cutting dynamics, thermal heat-affected zones (HAZ), and European CE compliance requirements for global industrial procurement.
Oxyfuel flame cutting remains the most economically viable process for cutting and beveling thick carbon steel plates ranging from 25 mm up to 300 mm and beyond. The process relies on pure oxygen reacting chemically with preheated iron at its ignition temperature (approximately 870°C to 900°C) to form iron oxide in an exothermic reaction.
Unlike plasma or laser processes which melt the substrate, oxyfuel cutting literally burns the steel away. The purity of the cutting oxygen stream is critical: a drop in oxygen purity from 99.5% to 98.5% reduces cutting speed by up to 25% and increases gas consumption exponentially. CE-certified torches feature optimized injector mixing chambers that preserve laminar flow at supersonic nozzle exits.
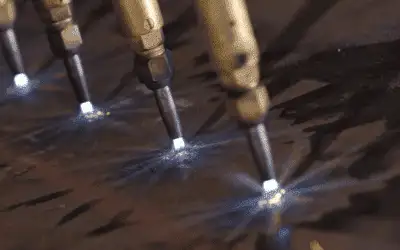
Every oxyfuel torch exported under CE certification undergoes rigorous hydrostatic pressure, thermal resistance, and burst testing according to EN ISO 5172 standards, ensuring zero gas leaks under high-volume industrial duty cycles.
Safety is paramount in high-pressure thermal cutting. Certified systems incorporate dual internal flashback arrestors and thermal shut-off valves that instantly arrest backfire flame fronts exceeding 1,000 meters per second.
For hazardous processing plants and offshore applications, pneumatic cold-cutting bevelers and oxyfuel gantry carriages adhere to ATEX equipment directives for safe operation in explosive gas environments.
Compare process economics, plate thickness capabilities, edge bevel quality, and operational cost metrics across industrial thermal and cold-cutting technologies.
| Cutting / Beveling Process | Optimal Thickness Range | Cutting Speed (100mm Plate) | Weld Edge Quality & Bevel | Heat-Affected Zone (HAZ) | Capital Expenditure |
|---|---|---|---|---|---|
| Oxy-Acetylene Flame | 25 mm – 300 mm+ | 250 – 350 mm/min | Good (Square / V / K Bevels) | Moderate to High (1.5–3.0 mm) | Economical / Low |
| Oxy-Propane / Natural Gas | 50 mm – 400 mm | 200 – 300 mm/min | Smooth cut face, low slag | Moderate (1.2–2.5 mm) | Low Operating Cost |
| High-Definition Plasma | 3 mm – 80 mm | Not Recommended >80mm | Laser-like on mid-plate | Minimal (0.2–0.5 mm) | Moderate to High |
| CNC Mechanical Bevel Milling | 6 mm – 60 mm | 500 – 1200 mm/min | Machined Precision (Zero Bevel Error) | Absolute Zero (Cold Process) | Moderate |
| Pneumatic Split-Frame Clamshell | Schedule 40 – 160 Pipe | Cold Pipe Cutting & Beveling | Machined Compound Bevel | Absolute Zero (Cold Process) | High ROI for On-Site Pipelines |
Insights into smart multi-torch integration, hydrogen hybrid fuels, automated multi-axis bevel heads, and digitized gas supply control systems.
Global fabricators are phasing out manual torch angle adjustments in favor of CNC-controlled triple-torch oxyfuel beveling heads. These systems automatically adjust V, X, Y, and K-bevel angles dynamically during gantry travel, slashing fit-up times for heavy bridge and vessel construction.
Driven by global carbon reduction mandates, industrial gas infrastructure is transitioning toward green hydrogen-oxygen blends and high-thermal MAPP gas mixtures. Advanced CE certified torches are pre-engineered with specialized mixing nozzles capable of handling higher hydrogen flame speeds.
Procurement directors increasingly demand integrated proportional gas valves and capacitive height control. Real-time telemetry logs preheat oxygen, fuel gas pressure, and standoff height data, ensuring batch-to-batch consistency and predictive wear alerts for torch tips.
Built on 35+ years of British engineering heritage in Nottingham, UK, our manufacturing operations combine in-house CNC machining, certified welding, and complete system assembly under one roof.
We do not rebadge third-party structures. From gantry machining and electrical panel wiring to torch height controller calibration, every machine is fully built and cut-tested in our facility before international dispatch.
As an authorized OEM partner for world-class cutting technology, our dual-process gantries pair heavy-duty oxyfuel torches with Hypertherm XPR plasma systems, delivering unmatched cutting range from 1 mm to 300 mm.
With machines operating in over 30 countries across Europe, the Americas, Asia, and Australia, our employed service engineers provide fast remote CNC diagnostics, documented maintenance protocols, and next-day spare part shipments.
Every cutting table is engineered with multi-zone downdraft extraction channels connected to high-efficiency industrial dust collector units, meeting strict workplace safety exposure standards globally.
Technical answers to common engineering, CE safety compliance, export logistics, and operation questions from international equipment buyers.
Whether you require a multi-head CNC oxyfuel gantry machine, a portable plate beveler, or an explosion-proof pneumatic cold-cutting split frame, our application engineers will analyze your CAD drawings and recommend the most profitable equipment setup.
