| Optimal Thickness Range | 3 mm to 50 mm (Piercing)
Severance to 80 mm | 0.5 mm to 20 mm (Ideal < 12 mm) | 25 mm to 300 mm (Carbon steel only) |
| Capital Equipment Cost (CapEx) | Moderate (£60k – £180k complete table) | High to Very High (£150k – £500k+) | Economic (£40k – £100k) |
| Tolerance to Rust & Mill Scale | Exceptional: Cuts through dirty, rusted, painted, or mill-scale plate effortlessly. | Poor: Requires clean, shot-blasted, or pickled plate surfaces to prevent beam scattering. | High: Flame heating burns off surface oxides prior to cutting arc. |
| Edge Quality (ISO 9013) | Class 2 – Class 4 (Near-laser bevel < 2°) | Class 1 – Class 2 (Perpendicular < 1°) | Class 3 – Class 5 (Slight top edge rounding) |
| Consumable Operating Cost | Low: Copper nozzles, electrodes, swirl rings (recyclable copper). | Moderate: Protective windows, ceramic rings, high-pressure N2 assist gas. | Very Low: Cutting tips, preheat gases (Propane/Acetylene + O2). |
| Assist / Shield Gas Demands | Shop Compressed Air, O2, N2, H35 (Compressed air drastically reduces cost). | High-Pressure Pure Nitrogen (20-30 bar) or Pure Oxygen. High gas costs. | Oxygen + Fuel Gas (Acetylene, Propane, Natural Gas). |
| Best-Fit Industry Sectors | Steel Service Centers, Heavy Structural Steel, Earthmoving Equipment, Marine Fabrication. | Precision Enclosures, Electronics, Thin Sheet HVAC, High-Tolerances Parts. | Heavy Shipyards, Offshore Wind Towers, Mining Machine Frames, Thick Plate Mills. |
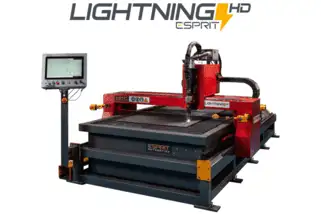 Flagship HD