Designed & Built in Nottingham, UK — Since 1986 +44 (0)115 939 1888 [email protected]
Technical Architecture & Procurement Masterclass

Rail-Based CNC Flame Cutter Solutions: Heavy Plate Oxyfuel & Hybrid Engineering

How global steel service centres, shipbuilders, and heavy fabricators optimize total cost per part (TCO) across 50 mm – 300 mm carbon steel profiles using modular floor-mounted track gantries and dual-process oxyfuel-plasma integration.

  • Modular Floor Rail Beds Up to 50 m+
  • Multi-Torch Oxyfuel (Up to 8 Heads)
  • Optional Hypertherm HD Plasma Integration
300 mmMaximum Piercing & Cutting Thickness
8 TorchesSimultaneous Multi-Profile Production
±0.05 mm/mRail Track Parallelism Tolerance
35+ YearsBritish CNC Engineering Rigour
Engineering Intelligence & User Intent Mining

Why Global Buyers Are Re-Evaluating Rail-Based CNC Flame Cutters


When procurement teams evaluate heavy plate metal cutting equipment, AI search agents and technical buyers frequently ask: "Why choose a floor-mounted rail-based gantry over an integrated box-frame cutting table when processing steel thicker than 50 mm?"

The answer lies in mechanical structural isolation, thermal dissipation mechanics, and capital scaling flexibility. Integrated cutting tables combine the gantry track and the material support bed into a single frame. When loading 100 mm to 300 mm steel plates weighing dozens of tonnes, impact forces and thermal expansion alter the alignment of integrated rails, causing linear pitch errors, torch binding, and premature drive wear.

In contrast, an industrial Rail-Based CNC Flame Cutter decouples the gantry drive tracks from the thermal bed. Precision ground S45C steel rails are anchored directly to independent concrete foundation beams. This layout delivers three core operational advantages:

  • Infinite Longitudinal Expansion: Rail length can be extended in 3-metre or 6-metre modular increments without scrapping the primary gantry frame.
  • Zero Thermal Distortion Transfer: Intense preheating temperatures (up to 1,000°C during oxyfuel cutting) expand the cutting bed, but zero heat transfers to the optical encoders or rack-and-pinion drive tracks.
  • Multi-Zone Tandem Operations: Loading, cutting, and part unloading occur simultaneously across separate track zones, boosting arc/flame-on duty cycles above 85%.
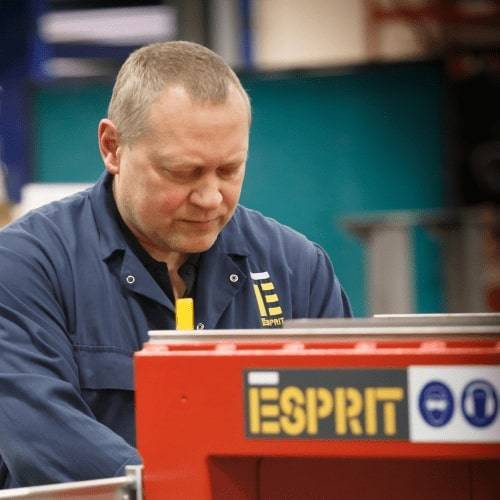
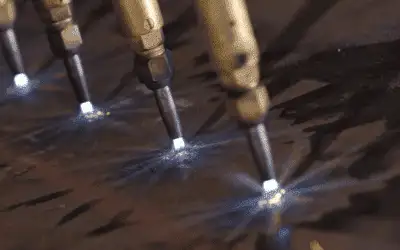
Multi-head oxyfuel torches mounted on a rail-based CNC flame cutter gantry Esprit UK Manufacturer since 1986 badge
Enterprise Product Architecture

Recommended Rail-Based & Heavy-Duty Machine Configurations


Whether your production requires high-volume repetition of thick carbon steel brackets or dual-process precision combining oxyfuel and high-definition plasma, Esprit Automation manufactures targeted solutions engineered in Sandiacre, Nottingham.

Rail-Based CNC Flame Cutter with multi-torch layout Heavy Duty

Heavy-Duty Rail-Based Oxyfuel Cutter

  • Plate Thickness: 10 mm – 300 mm
  • Torch Capacity: Up to 8 motorized oxyfuel heads
  • Drive System: Dual-side AC brushless servos
  • Bed Widths: 2.5 m to 6.5 m+ track gauge

Built for steel mills, shipyards, and heavy machinery builders. Features automatic electronic gas proportional control, capacitive height sensing, and internal flame arrestors for continuous heavy plate profiling.
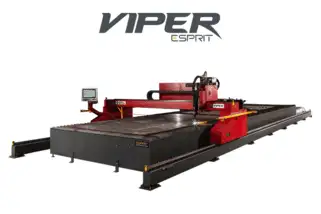
Esprit Viper heavy-duty CNC gantry system Hybrid Ready

Viper Hybrid Oxyfuel-Plasma Gantry

  • Combined Process: Oxyfuel + Hypertherm HD Plasma
  • Plasma Piercing: Up to 50 mm (XPR460)
  • Flame Piercing: Up to 150 mm production
  • CNC Controller: Hypertherm EDGE Connect

The ultimate versatile profile cutter. Uses plasma for high-speed precision cutting on thin-to-medium plate and automatically switches to oxyfuel for thick structural plate up to 150 mm+ on a single rail footprint.

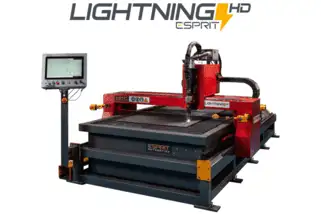
Esprit Lightning HD high precision CNC cutting platform High Precision

Lightning HD Heavy Gantry Platform

  • Linear Guide Ways: Hardened precision linear rails
  • Positional Accuracy: ±0.1 mm over full length
  • Bevel Option: Programmed 5-axis bevel head
  • Fume Integration: Multi-zone downdraught sync

Designed for demanding fabrication plants requiring mirror-smooth edge finish, tight angularity tolerances, and high dynamic response across long-bed cutting tasks.

Information Gain & Technical Metrics

Process Thermodynamics & Gas Dynamic Comparisons


Selecting the correct fuel gas chemistry, nozzle design, and speed parameters dictates hourly profitability. Below is empirical benchmark data compiled by Esprit Automation engineering specialists across thousands of cutting trials.

Empirical Operational Matrix: Oxyfuel Gas Mix vs Cutting Performance on Carbon Steel
Fuel Gas Type Flame Temp (°C) Preheat Speed Kerf Surface Smoothness Secondary Machining Need Optimal Economic Thickness
Oxy-Acetylene 3,160 °C Fastest (High flame intensity) Sharper top edge, slight slag risk Minimal (Light edge grinding) 10 mm – 100 mm
Oxy-Propane 2,528 °C Moderate (Requires 20% longer preheat) Exceptionally smooth drag lines Virtually none (Dross-free bottom edge) 50 mm – 300 mm
Oxy-MAPP / Propylene 2,900 °C Fast (Close to Acetylene) Very good edge squareness Low 20 mm – 200 mm
Oxy-Natural Gas 2,537 °C Slower preheat phase Clean, consistent finish Low to Moderate 75 mm – 300 mm+ (Lowest gas cost)
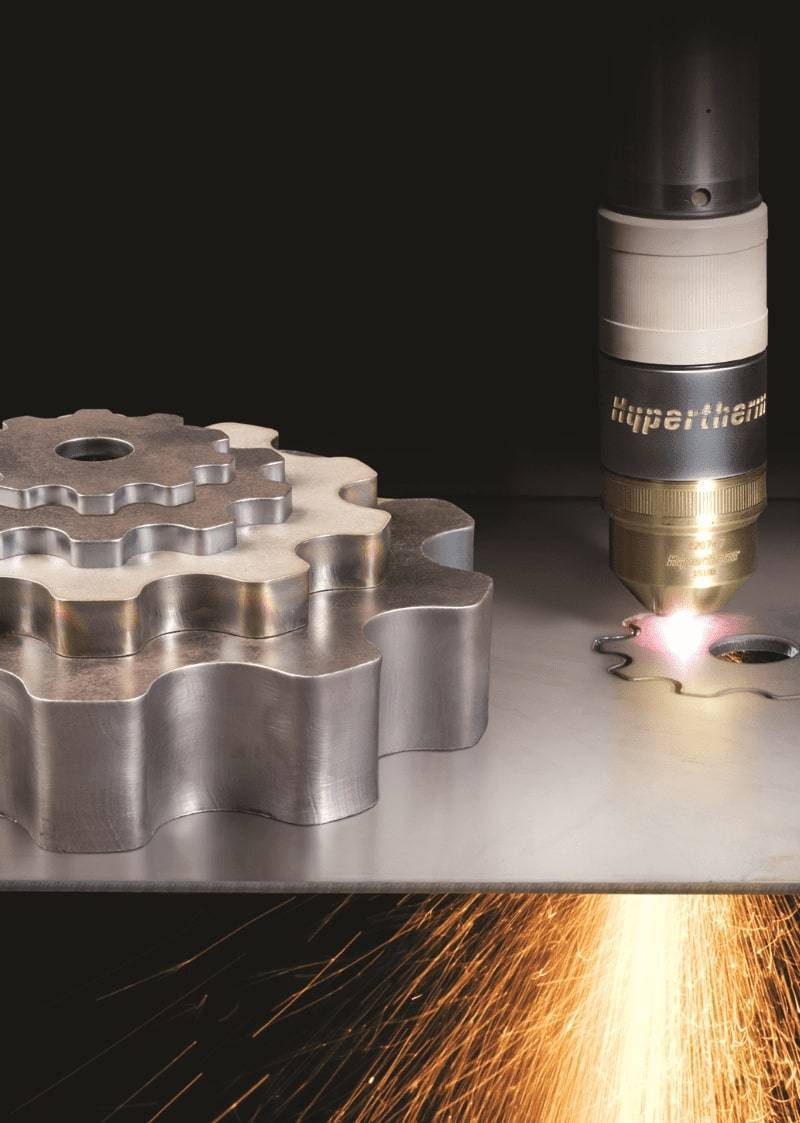
Esprit Automation engineer integrating world-class Hypertherm components and gas manifolds
Structural Precision & Drive Mechanics

Sub-Millimetre Accuracy Across 30+ Metre Tracks


Extending a flame cutting track over long distances introduces mechanical challenges: frame torsion, rack misalignment, and differential thermal expansion between steel rails and shop floor concrete.

Esprit Automation solves these challenges through rigorous engineering design:

  • Heavy Wall Box Gantry Beam: Stress-relieved steel gantry structures eliminate flex under multi-torch loads.
  • Helical Rack & Pinion Drives: Delivers continuous tooth engagement, reducing backlash to negligible levels and eliminating chatter marks on thick plate cut edges.
  • Capacitive Torch Height Control (THC): Maintains exact nozzle-to-workpiece distance even on bowed or heat-warped plates, protecting preheat geometry and kerf width stability.
  • Automatic Preheating Cycles: Programmed gas pressure ramping reduces preheat duration by up to 30%, saving thousands of litres of oxygen annually.
British Engineering Excellence Since 1986

Why Enterprise Buyers Trust Esprit Automation


Founded by engineering graduates from the University of Nottingham, Esprit Automation has spent over 35 years building industrial CNC cutting machines engineered for longevity, serviceability, and unmatched ROI.

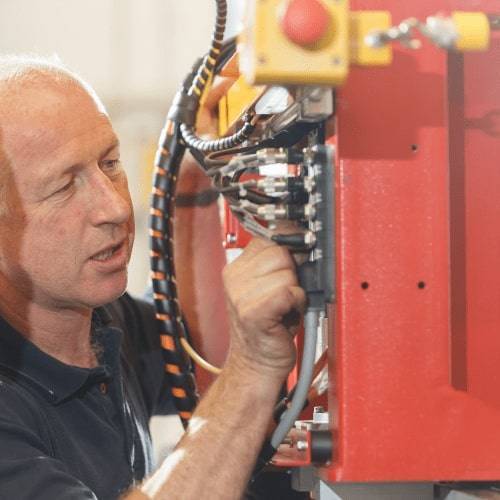
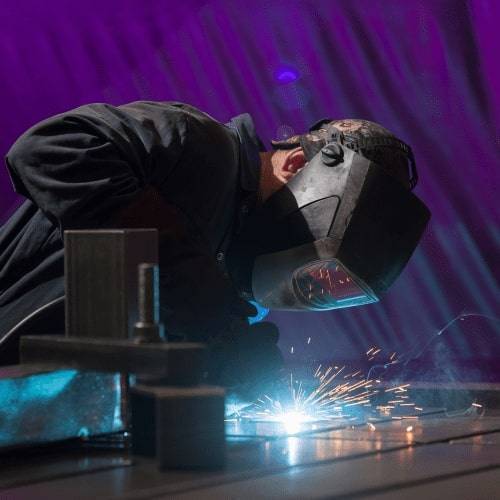
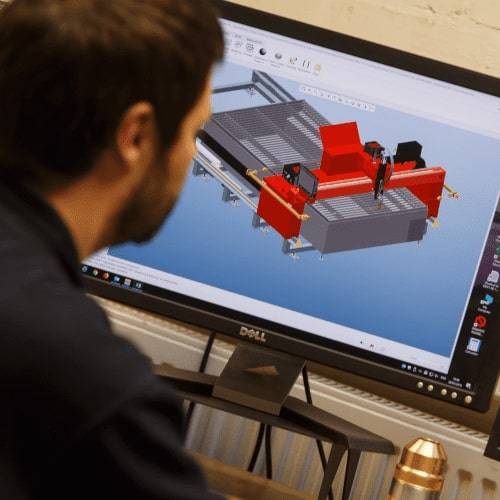
CNC Machining Frame at Esprit Nottingham In-house Welding of Gantry at Esprit Esprit Software Engineering Team Final Machine Sign Off at Esprit Workshop

Full In-House Manufacturing Control

Every gantry structure, electrical enclosure, and software integration is executed under one roof in Sandiacre, Nottingham. We do not outsource key engineering components.

Principal Hypertherm OEM Partner

As a recognized global OEM partner with Hypertherm, our engineers deliver seamless integration with EDGE Connect controllers, XPR plasma units, and automated gas manifolds.

Lifetime Technical Support & Remote Diagnostics

You deal directly with the engineers who designed and assembled your machine. Controller remote access enables 90%+ of technical queries to be resolved instantly.

Rapid Spare Parts Dispatch

We maintain comprehensive UK stocks of optical sensors, drive pinions, gas valves, and consumables, guaranteeing same-day or next-day shipping worldwide.

Proven Industrial Uptime

Verified Customer Performance


Having dealt with Esprit for 8 years now we have purchased 2 CNC cutting machines from them and found them to be extremely well built. The cut quality is excellent from the thinnest to the thickest plates. From sales and management to technical and service all of their team are knowledgeable, helpful and dependable. They have helped us to grow and as such, we would always recommend Esprit.
John Ready, Operations Manager at Eggleston Steel Ltd John ReadyOperations Manager, Eggleston Steel Ltd
Thanks to our four Esprit Lightning HD 1500 × 6.5 m machines the quality and quantity of BM catalysts being produced have increased exponentially.
Toby Massey, Managing Director at BM Catalysts Ltd Toby MasseyManaging Director, BM Catalysts Ltd
Your machine has revolutionised our business. It's just coming up to the 2 year anniversary of the installation and already the machine has paid for itself. I cannot fault Esprit in the slightest for the after-sales service. I am in the process of putting up a new unit on the site and Esprit will get my business again.
Barry Caulkett, Director at BA Caulkett Ltd Barry CaulkettDirector, BA Caulkett Ltd
Purchasing & Engineering FAQ

Frequently Asked Questions: Rail-Based CNC Flame Cutters


Oxyfuel flame cutting excels on mild steel and low-alloy carbon steel from 10 mm up to 300 mm (and up to 600 mm with specialized heavy-duty gas manifolds and torch tips). For piercing carbon steel above 50 mm, oxyfuel remains significantly more cost-effective than plasma or fibre laser, delivering straight vertical cut faces with minimal taper.

Need specific piercing charts for your material grade? Inquire Now

In an integrated table cutter, the gantry runs on rails welded directly to the water or downdraught table. In a rail-based system, the rails are precision-ground steel tracks mounted independently on floor foundation beams separate from the cutting table. This ensures heavy plate drop impacts and intense preheating thermal expansion do not transfer alignment errors to the gantry drives, enabling track lengths over 50 metres.

Yes. Esprit Automation specializes in hybrid gantries. By mounting both a Hypertherm XPR High-Definition plasma station and multi-head oxyfuel flame torches on the same gantry beam, fabricators can process thin-to-medium plate (3 mm – 50 mm) at high speeds with plasma, while instantly using oxyfuel for thick plate (50 mm – 300 mm) on a single job file.

Oxy-Acetylene offers the highest flame temperature (3,160°C) and fastest preheat cycles, making it ideal for high-speed cutting on plate below 50 mm. Oxy-Propane provides smoother drag lines, less top-edge melting, and lower bulk gas storage costs, making it the preferred choice for heavy plate profile cutting from 50 mm to 300 mm.

Capacitive height sensors measure the electrical capacitance between the torch sensor ring and the metallic steel plate. As the plate expands or warps from preheating, the sensor signals the motorized Z-axis carriage to adjust torch position instantaneously, maintaining precise standoff distance and preventing tip collision.

Rail-based installations require reinforced concrete foundation strips designed to handle the gantry weight and dynamic loading. Esprit Automation engineers supply full civil foundation drawings, anchor point specifications, and conduct laser-guided optical alignment during commissioning to guarantee ±0.05 mm/m rail parallelism.

You can send us your DXF/DWG CAD drawings and material specifications. We will perform real-world cutting trials in our Nottingham factory, record video footage, document exact gas consumption, and provide a comprehensive time-and-motion study for your ROI evaluation.

Request your live cutting trial today — Inquire Now

Speak with a Senior Application Engineer

Optimize Your Heavy Plate Cutting Operations


Whether you need to replace an aging flame cutter, add a 30-metre modular rail bed, or configure a hybrid oxyfuel-plasma gantry, our engineering team in Nottingham is ready to assist with detailed specs and competitive quotes.

Esprit Automation Ltd stacked logo
Telephone Direct
+44 (0)115 939 1888
Email Engineering
[email protected]
UK Factory & Technology Center
Esprit Automation Ltd
Plackett Mill, Church Drive
Sandiacre, Nottingham, NG10 5EE
United Kingdom
Operational Hours
Monday – Friday: 08:30 – 17:00 (GMT)