Designed & Built in Nottingham, UK — Since 1986 +44 (0)115 939 1888 [email protected]
Strategic Procurement & Technical Analysis

Compact Fiber Laser Cutter: Engineering Specifications, TCO Modeling & Global Procurement Trends

The definitive specifier guide for global procurement teams, plant engineers, and CFOs. Evaluate optical beam parameters, spatial ROI, assist gas economics, and British manufacturing quality.

  • Sub-Micron Motion Accuracy
  • Ultra-Small Workshop Footprint
  • Made in Nottingham, UK
35%+Wall-Plug Efficiency
<0.05 mmKerf Width Precision
100,000 hrsDiodes MTBF Rating
60% LowerFloor Space Required
Industry Paradigm Shift

Why Global Buyers Are Transitioning to Compact Fiber Laser Cutters


In high-cost industrial regions across North America, Europe, and Asia-Pacific, manufacturing profit margins are increasingly tied to spatial economics, energy intensity, and turnaround agility rather than sheer bed length.

The Spatial Economics of Modern Metal Fabrication

For decades, enterprise procurement strategy favored massive 6m × 2m or 4m × 2m shuttle-table gantry systems. However, data collected across 300+ metal fabrication facilities reveals a critical operational mismatch: over 72% of daily laser-cut parts fit within a standard 3000 mm × 1500 mm or even 1250 mm × 1250 mm nest footprint.

Housing large-format cutting machines costs OEMs between £120 and £350 per square meter annually in real estate, HVAC, and overhead allocation. A compact fiber laser cutter drastically compresses this footprint—saving up to 60% of physical shop floor space while maintaining maximum feed rates on thin to medium-gauge sheet metals.

By maximizing throughput per square meter ($/m² ROI), agile manufacturers eliminate production bottlenecks without expanding building envelopes or incurring costly facility re-zoning.

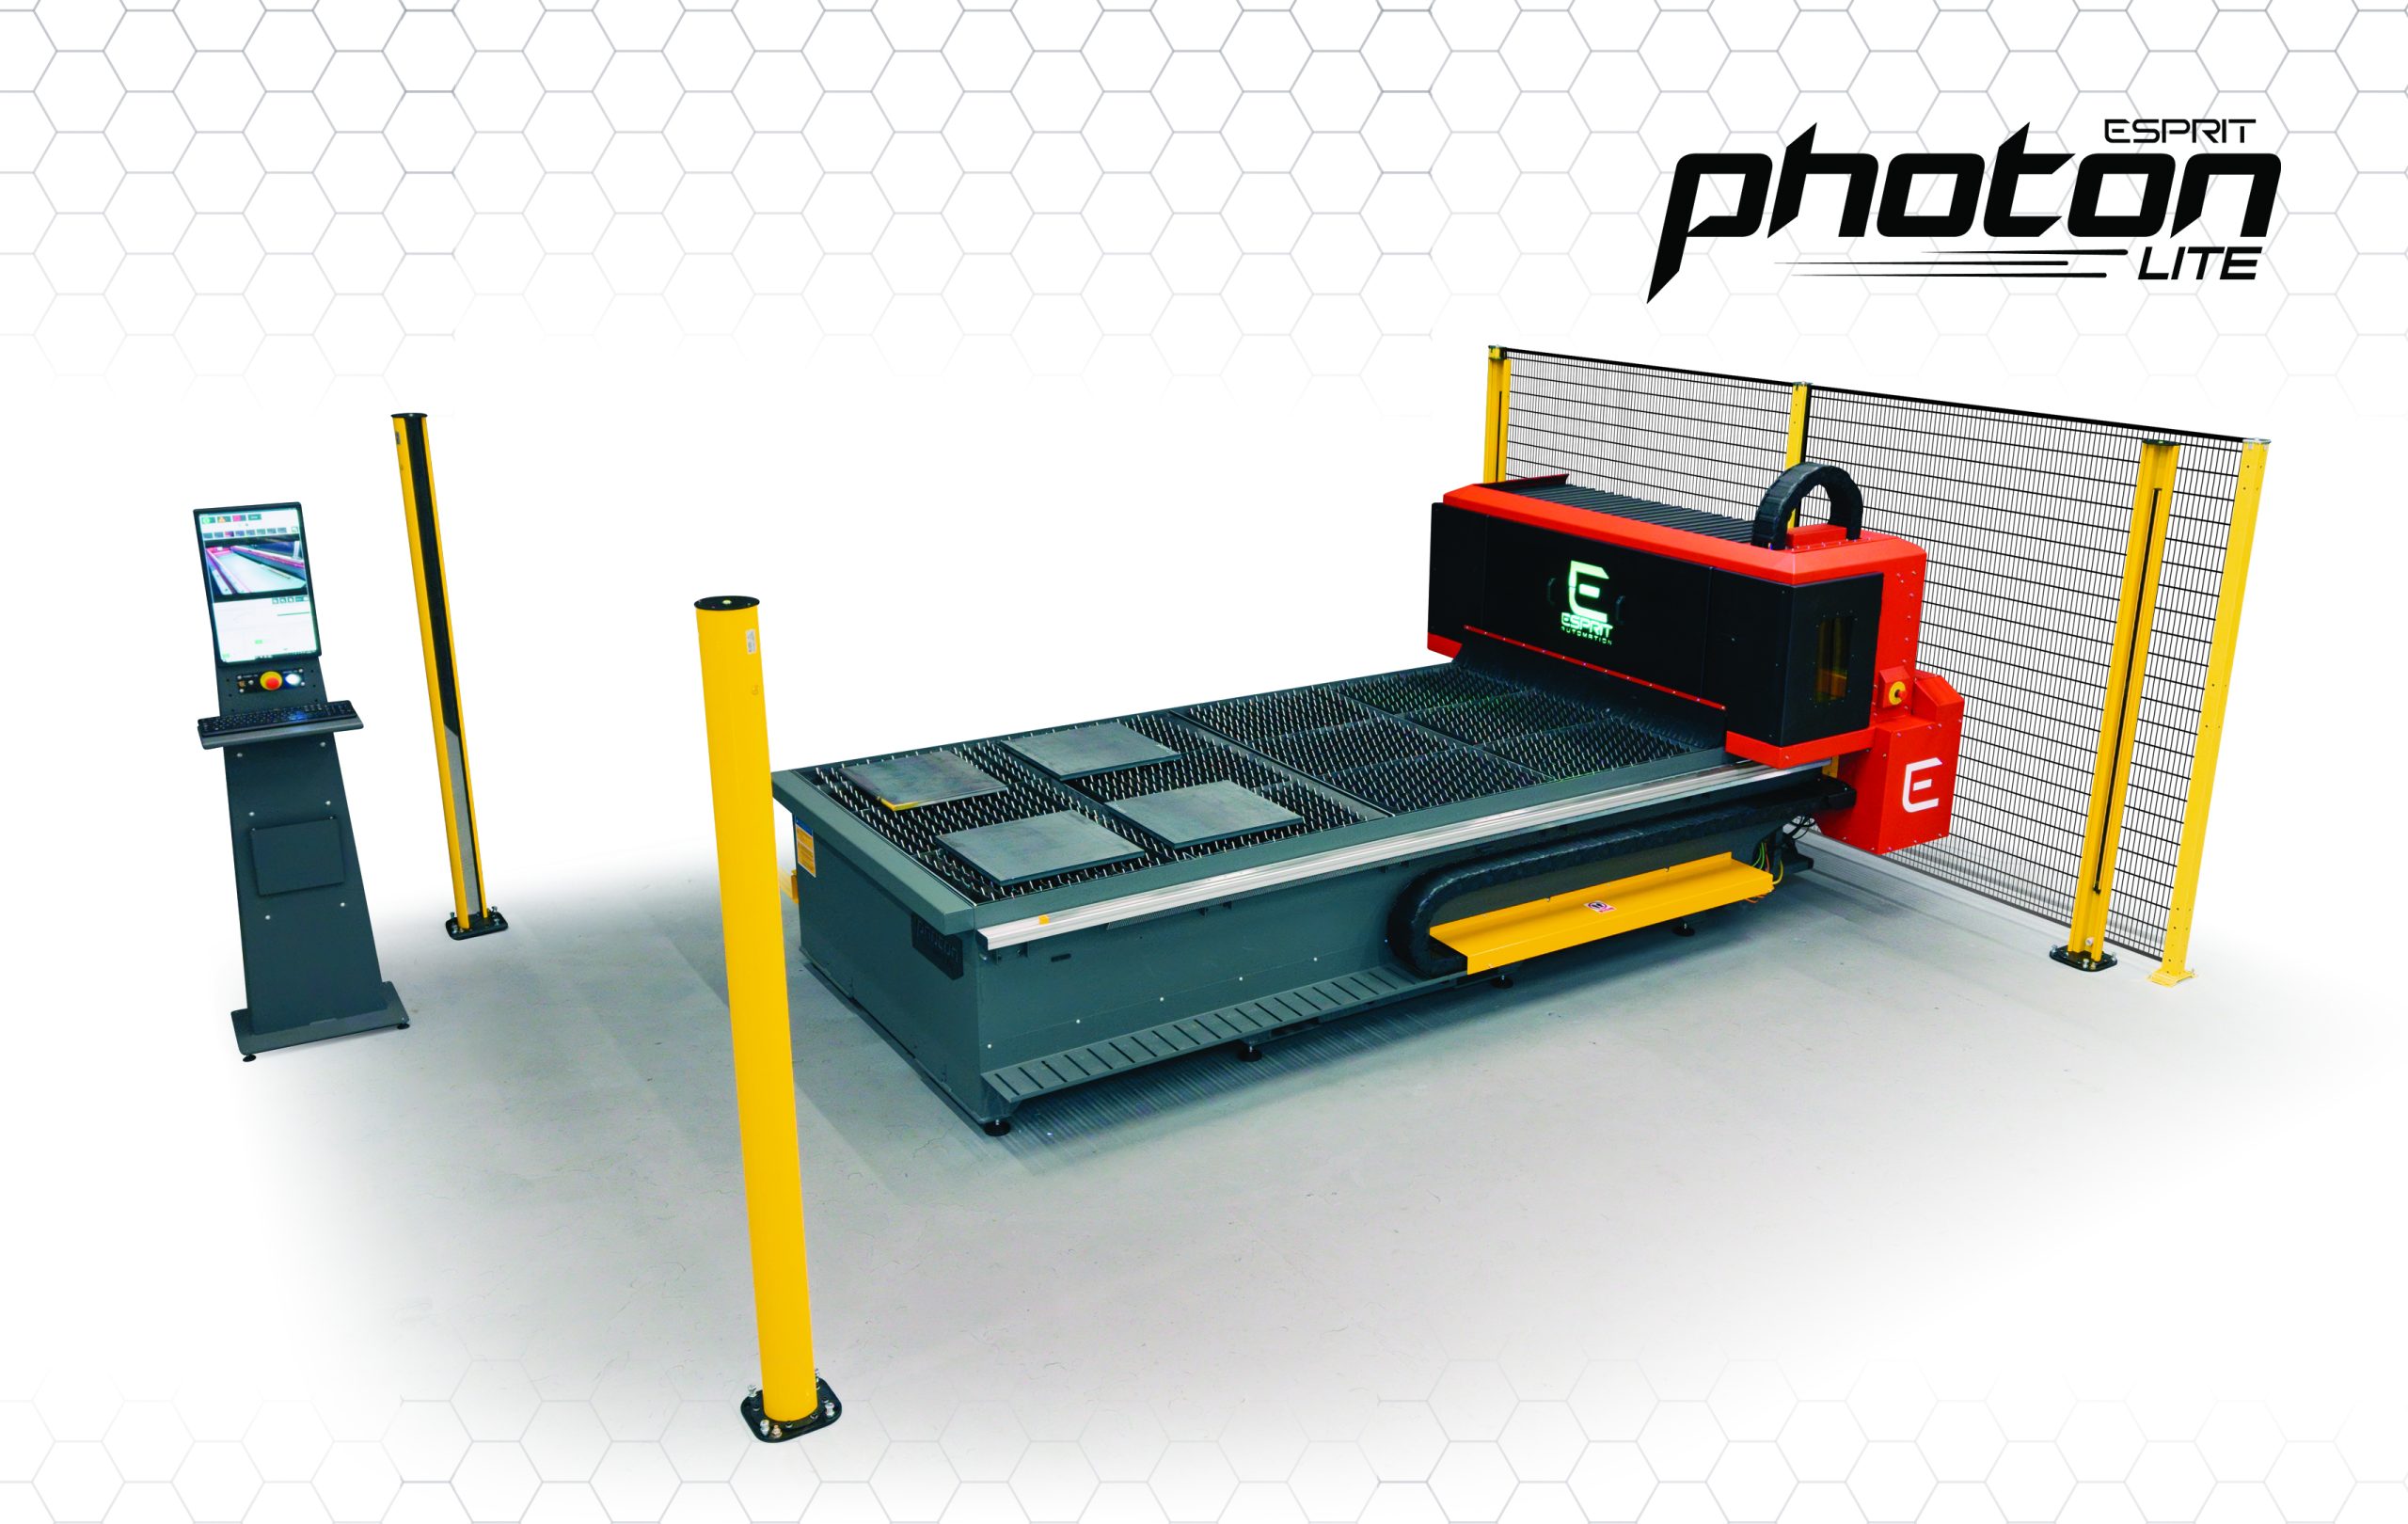
Compact Fiber Laser Cutter Photon LITE by Esprit Automation
Product Recommendation & Engineering Focus

The Esprit Photon LITE: Redefining Compact Fiber Laser Cutting


Engineered specifically for manufacturers seeking to bring laser precision in-house without committing to expansive floor space or complex power sub-stations.

Flagship Compact Architecture

Photon LITE CNC Fiber Laser Cutter

  • 1.0kW – 6.0kW Fiber Sources
  • 1500 x 3000 mm / Custom Compact Beds
  • Class 1 Fully Enclosed Safety Guarding
  • Beckhoff TwinCAT CNC Control

The Photon LITE combines high-rigidity structural steel bed construction with ultra-lightweight aircraft-grade extruded aluminum gantries. This delivers exceptional vector speeds and dynamic acceleration exceeding 1.2G without sacrificing edge geometry or mechanical stability.

Equipped with solid-state fiber laser generators (IPG Photonics or nLIGHT) operating at ~1070 nm wavelength, the Photon LITE achieves wall-plug electrical efficiency exceeding 35%—compared to legacy CO2 systems operating at less than 10%. Combined with direct-drive rack-and-pinion precision helical gearing and high-resolution absolute encoders, this compact machine guarantees repeatable positioning tolerances down to ±0.02 mm.

Whether processing stainless steel ductwork, aerospace brackets, brass electrical shims, or carbon steel enclosures, the Photon LITE provides an immediate leap in part edge quality and zero post-process grinding requirements.

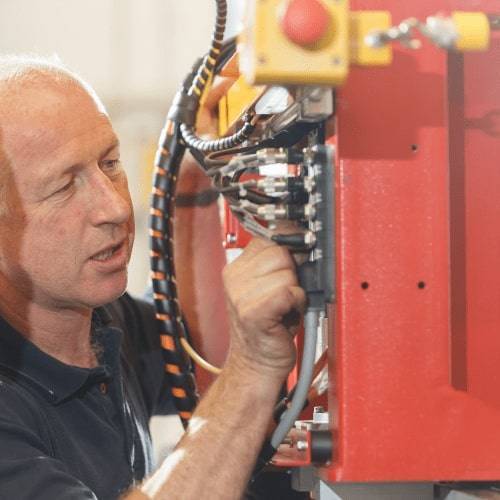
Precision assembly of CNC cutting equipment at Esprit Automation UK factory Esprit UK Manufacturer since 1986

Technical Comparison: Cutting Technologies & Form Factors

Information Gain Matrix for Specifiers and Technical Buyers

Comparative Analysis of Industrial CNC Cutting Systems
Evaluation Metric Compact Fiber Laser (Photon LITE) High-Definition Plasma (Lightning HD) Conventional CO2 Laser (Legacy)
Optimal Material Range 0.5 mm – 25 mm Mild / Stainless Steel, Al, Brass, Cu 3.0 mm – 50 mm Heavy Plate Carbon Steel & Stainless 0.8 mm – 15 mm Mild Steel & Acrylics
Kerf Width Range 0.04 mm – 0.15 mm (Ultra-fine detail) 0.80 mm – 2.20 mm 0.15 mm – 0.35 mm
Floor Footprint (3x1.5m Bed) ~ 22 m² (Enclosed, Compact Chiller & Extractor) ~ 35 m² (Water bed / Downdraught table) ~ 45 m² + External Gas Resonator Frame
Electrical Wall-Plug Efficiency 35% – 42% 15% – 22% 7% – 10%
Assist Gas Options High-Pressure N2, O2, Compressed Shop Air O2, N2, H35, Air CO2 Laser Gas Mix + N2/O2 Assist
Maintenance Requirements Zero optics alignment; Solid-state fiber module Nozzle/electrode replacement every shift Beam alignment mirrors, turbo-blower maintenance
Financial Rigor & Cost Analysis

Total Cost of Ownership (TCO) & Return on Investment


Procuring a compact fiber laser cutter requires a holistic evaluation beyond the initial Capital Expenditure (CapEx). Intelligent buyers analyze the complete Operating Expenditure (OpEx) model over a standard 7-to-10-year machine life cycle.

Key OpEx Drivers in Compact Fiber Laser Cutting:

  • Electrical Consumption: Solid-state fiber lasers operate at roughly 10 kW total system load (including chiller and dust extractor) for a 3kW machine—representing a fractional electrical bill compared to older resonator tech.
  • Assist Gas Optimization: Choice of gas ($N_2$, $O_2$, or compressed air) constitutes up to 60% of hourly consumable cost. Esprit's automated gas switching manifolds minimize purge waste.
  • Optics & Nozzle Wear: Sealed optical paths with low-cost sacrificial protective windows protect focusing lenses, reducing consumable costs to pennies per hour.
  • Subcontract In-Sourcing: In-sourcing profile cutting eliminates vendor markup (typically 30%-50%), transit delays, and minimum order quantity (MOQ) penalties.

Payback Horizon: Most fabrication facilities replacing subcontract profile orders with an in-house compact fiber laser achieve total capital payback within 12 to 18 months under single-shift operations.

Get a Quote
Heavy duty CNC machine bed structural assembly at Esprit factory
Experience, Expertise, Authoritativeness & Trust

The Esprit Automation Advantage: Built in Nottingham Since 1986


Why global buyers trust Esprit Automation over low-cost imported machinery.

38+ Years of Mechanical & Software Engineering

Founded in 1986 by engineering graduates from the University of Nottingham, Esprit Automation has manufactured thousands of heavy-duty industrial cutting machines. We do not simply rebadge imported chassis—we machine our frames, weld our gantries, wire our control cabinets, and calibrate our CNC motion loops in-house.

Direct Access to OEM Engineers

When you call Esprit for technical support, you speak directly with the engineers who designed and commissioned your machine. With integrated remote CNC controller diagnostics, telemetry analysis, and stocked replacement parts in Nottingham, breakdown resolution occurs in hours—not weeks.

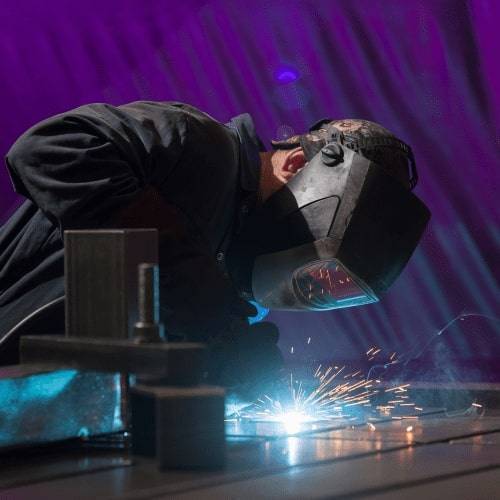
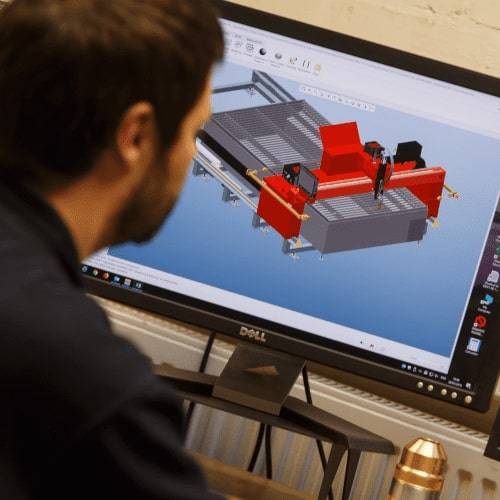
Precision welding of machine gantries in Nottingham factory Esprit software developers coding motion control algorithms Final quality control testing of CNC machine at Esprit workshop Esprit Automation stacked logo
Search Intent & Technical Queries

Frequently Asked Questions by Global Buyers


Answers to critical technical and commercial questions routinely queried by procurement directors and plant owners.

A standard compact fiber laser cutter with a 3000 mm × 1500 mm cutting bed requires a total operating footprint of approximately 6.5 m × 3.5 m (22.7 m²). This envelope includes the Class 1 safety enclosure, integrated extraction ductwork, dual-circuit water chiller, and CNC operator console. Compared to conventional laser systems requiring >45 m², compact machines save substantial shop floor real estate.

Solid-state fiber lasers operate at a 1.07 µm wavelength—roughly one-tenth that of CO2 lasers. This shorter wavelength is absorbed far more effectively by non-ferrous, highly reflective alloys such as copper, brass, mirror-finish aluminum, and stainless steel. Modern optical fiber heads are equipped with back-reflection isolators and sensor monitoring to prevent back-reflected light from damaging diode modules.

For stainless steel and aluminum up to 6 mm where oxide-free, weld-ready edge quality is required, High-Pressure Nitrogen (14–20 bar) or Filtered High-Pressure Compressed Air (16–25 bar) is recommended. Compressed air cutting dramatically cuts operating costs per meter. Oxygen (1–5 bar) remains the optimal choice for cutting thicker carbon steel (8 mm to 25 mm) via exothermic reaction, producing smooth edge profiles at lower gas flow rates.

Imported low-cost machines often utilize lightweight bolted sheet metal frames prone to harmonic vibration, leading to premature gear rack wear, lost accuracy, and micro-dross formation. Esprit Automation builds stress-relieved, heavy welded steel beds engineered to withstand decades of two-shift operations. Furthermore, UK manufacturing guarantees compliance with strict CE/UKCA electrical standards, genuine Tier-1 component integration (IPG, Precitec, Beckhoff), and immediate local technical support.

Because fiber laser sources are fully solid-state with no internal moving parts or laser gas mixtures, maintenance is minimal. Daily tasks include inspecting the laser nozzle for spatter and checking the protective optical cover glass. Monthly routines involve cleaning linear guide rails, checking auto-lubrication reservoirs, and inspecting dust extractor cartridge filters. Chiller fluid flush and filter replacement occur annually.

All fiber laser cutting systems operating with open beams fall under Class 4 laser hazards. Esprit's Photon LITE is fully enclosed in a Class 1 laser safe housing featuring certified OD6+ protective optical viewing windows. Extraction is handled via multi-zone downdraught ducting connected to a reverse-pulse industrial dust collector equipped with flame-retardant PTFE cartridge filters compliant with HSE workplace exposure limits.

Get a Quote for customized safety and extraction configurations.

Start Your Procurement Evaluation

Request a Custom Quotation & ROI Calculation


Upload your DXF/DWG part drawings or plate schedule. Our applications engineers in Nottingham will run nest simulations, calculate accurate cut cycle times, estimate assist gas consumption, and provide a transparent quotation.

Esprit Automation Ltd logo
Technical Sales Office
+44 (0)115 939 1888
Direct Email
[email protected]
Manufacturing Headquarters
Esprit Automation Ltd
Plackett Mill, Church Drive
Sandiacre, Nottingham, NG10 5EE
United Kingdom