Designed & Built in Nottingham, UK — Since 1986 +44 (0)115 939 1888 [email protected]
British Engineering Excellence · Global Procurement Standard

High-Definition Plasma Cutting System: Engineering Architecture & Technical Benchmark Guide

How global metal fabricators, steel service centres, and structural engineers achieve near-laser edge quality, ISO 9013 Range 2/3 bevel compliance, and up to 60% lower cost-per-part on 3 mm to 50 mm plate.

  • ISO 9013 Range 2 & 3 Cut Quality
  • Hypertherm OEM Principal Partner
  • In-House Engineering & CNC Software
1986UK Engineering Since
50 mmHD Production Pierce
ISO 9013Range 2/3 Edge Tolerance
30+Export Countries Supported
Global Procurement & Engineering White Paper

High-Definition Plasma Cutting System: Evaluating Edge Tolerances, Thermal Distortion, TCO, and Gas Dynamics for Next-Generation Industrial Metal Fabrication


For modern industrial procurement managers, structural steel fabricators, and OEM metal processors, selecting a High-Definition Plasma Cutting System is no longer merely a decision about raw metal separation. It is an exercise in total cost of ownership (TCO) optimization, metallurgical edge integrity, and automated downstream process elimination. In an industrial landscape dominated by volatile electricity costs, skilled welder shortages, and demanding tolerance standards (such as EN 1090-2 and ISO 9013), high-definition plasma technology has emerged as the most profitable cutting process for mild steel, stainless steel, and aluminium across the 3 mm to 50 mm thickness window.

Esprit Lightning HD High Definition Plasma Cutting System
Physics & Technology Breakdown

What Defines a Genuine High-Definition Plasma Cutting System?

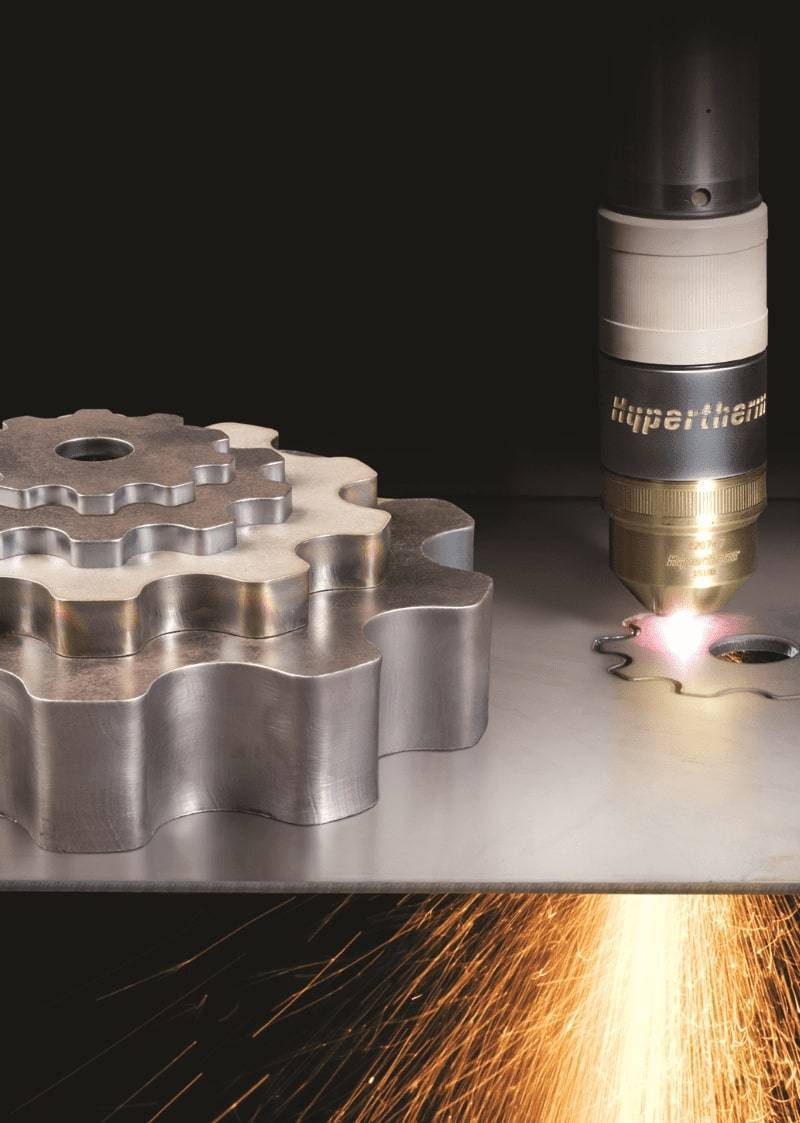
Conventional air plasma systems rely on unconstrained electric arcs passing through air or nitrogen nozzles, yielding cut edge bevel angles between 4° and 10°, substantial dross accumulation, and a wide kerf. Conversely, a true High-Definition Plasma Cutting System—such as the Esprit Lightning HD powered by Hypertherm XPR technology—utilizes extreme arc constriction, highly focused energy densities exceeding 60,000 amperes per square inch, and microprocessor-controlled shield gas shrouding.

This arc constriction produces an exceptionally narrow plasma column with uniform energy distribution. The resulting kerf approaches the narrow profile of fiber laser cutting while maintaining straight, bevel-free cut edges compliant with ISO 9013 Range 2 and Range 3 standards. Crucially, high-definition plasma preserves the chemical composition of the cut face, minimizing nitriding and hardening, which allows immediate robot welding without grinding.

  • Constricted Arc Geometry
  • Proportional Automatic Gas Console
  • Vented Water Shroud (VWI) Technology
  • True Hole Automated Execution
Comparative Process Engineering

Technical Process Matrix: High-Definition Plasma vs. Fiber Laser vs. Conventional Air Plasma

Global procurement teams frequently inquire whether high-power fiber laser systems render plasma obsolete. The definitive empirical data below demonstrates why high-definition plasma remains the uncontested economic champion for mid-to-heavy plate fabrication.

Empirical Comparison of Metal Cutting Processes on Mild Steel & Stainless Plate
Evaluation Metric High-Definition Plasma System (e.g., Esprit XPR300/460) High-Power Fiber Laser (12kW – 20kW) Conventional Air Plasma (Standard CNC Table)
Optimal Economic Thickness 3 mm to 50 mm (Production Pierce) 0.8 mm to 20 mm 1 mm to 25 mm
Capital Expenditure (CapEx) Moderate (Rapid ROI within 12–18 months) High to Very High (Heavy capital load) Low (Entry-level fabrication)
ISO 9013 Edge Bevel Range Range 2 to Range 3 (1° to 3° average bevel) Range 1 to Range 2 (0.5° to 1.5°) Range 4 to Range 5 (4° to 8° taper)
Tolerance to Surface Rust & Scale Exceptional (Cuts through mill scale, rust & primer easily) Poor (Requires pristine plate; surface rust causes beam bounce & lens contamination) High (Cuts raw plate but produces top dross)
Hole Quality (Bolt Diameter to Thickness) 1:1 Ratio True Hole Quality (Taper-free cylindrical holes ready for bolting) Superior small-diameter hole piercing (<1:1 ratio) Poor (Severe taper; requires secondary drilling)
Electrical Power Consumption 35 kW – 85 kW (Low idle energy draw) 45 kW – 110 kW (High total facility power draw) 20 kW – 40 kW
Consumable Operating Cost Low per metre (Hypertherm ArcGlide & CoolFlow technology) Low on thin sheet, extremely high assist gas cost (N2) on thick plate Low capital consumable cost, higher part scrap rate
Enterprise Machine Range

High-Definition Plasma Cutting Systems: Recommended Models


Engineered in Nottingham, UK, Esprit Automation’s high-definition plasma machines combine ultra-rigid mechanical structures with world-leading Hypertherm XPR power source integration.

Esprit Lightning HD High-Definition Precision Plasma Cutter Flagship Precision

Lightning HD High-Definition System

  • Dual precision helical rack & pinion drives
  • Linear recirculating ball bearings on all axes
  • Configured with Hypertherm XPR170 / XPR300 / XPR460
  • True Hole & True Bevel technology integrated

The Lightning HD is the definitive benchmark for high-speed, ultra-precision plate cutting. Designed specifically for structural steel fabricators and high-volume component manufacturers requiring continuous ISO 9013 Range 2/3 performance. Its heavy-duty box gantry eliminates dynamic deflection at high acceleration rates.
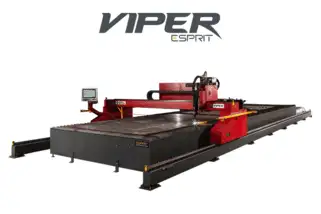
Esprit Viper Heavy-Duty High-Definition Plasma Cutting Table Heavy-Duty Steel

Viper HD Heavy-Duty Cutting System

  • Extra-heavy gantry structure for thick plate handling
  • Multi-shift continuous production duty cycle
  • Accepts dual plasma heads or oxyfuel combination
  • Fully zoned automatic downdraught extraction table

Built for steel service centers, heavy machinery manufacturers, and shipyards, the Viper HD delivers massive structural mass to withstand heavy plate loading up to 100 mm thick while maintaining micro-step high-definition torch positioning accuracy.

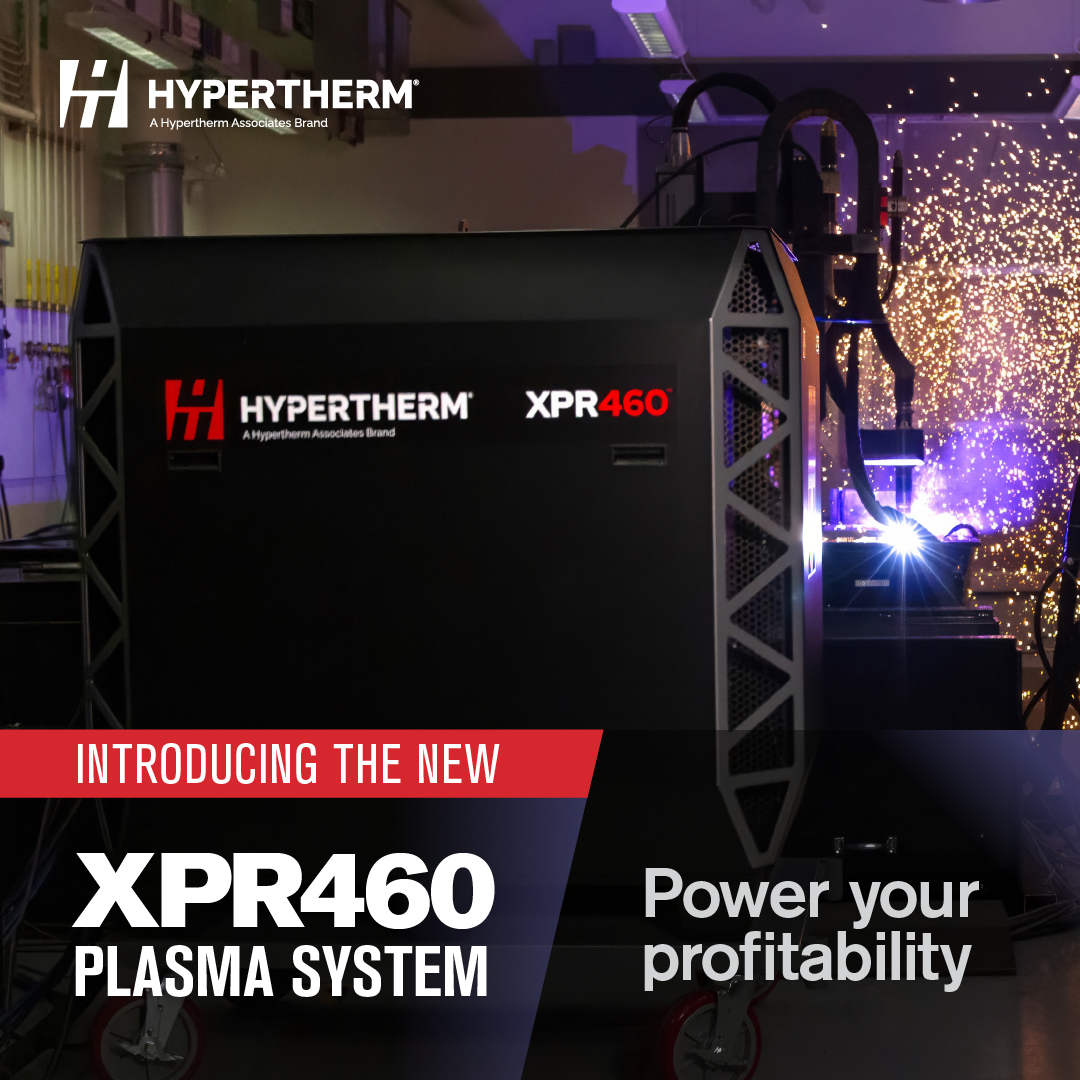
Hypertherm XPR460 Power Source on Esprit CNC Plasma System OEM Power Integration

Hypertherm XPR Power Source Series

  • XPR170, XPR300, and XPR460 gas options
  • X-Definition cut quality on mild steel & non-ferrous
  • Auto-gas console with automatic cut chart loading
  • Up to 50% longer consumable life via CoolFlow

As a principal UK OEM partner of Hypertherm, Esprit tightly integrates the XPR system with our custom CNC software, ensuring seamless communication between torch height control, gas dosing consoles, and gantry motion controllers.

Strategic Procurement Forecast

Future Development & Global Procurement Trends in High-Definition Plasma Cutting


As global manufacturing shifts toward Industry 4.0 automation, decarbonization, and supply-chain agility, the purchasing criteria for high-definition plasma cutting systems have fundamentally evolved. Overseas buyers and enterprise procurement officers must prepare for four pivotal industry developments.

1. AI-Driven Predictive Telematics & Consumable Life Optimization

Modern high-definition plasma systems are replacing manual operator intervention with real-time arc voltage telemetry, predictive consumable wear tracking, and AI-driven cut-chart adjustment. By continuously sensing micro-variations in coolant temperature, gas pressure, and arc voltage, modern Esprit CNC controllers automatically adjust torch height and pierce delay in real time. This prevents catastrophic torch collisions, eliminates part scrap due to worn nozzles, and extends consumable lifespan by up to 40% compared to legacy CNC plasma tables.

2. Re-balancing Total Cost of Ownership: HD Plasma vs. Fiber Laser

While fiber lasers dominated light-gauge sheet metal discussions over the past decade, high inflation in industrial electricity tariffs and expensive nitrogen assist gas prices have prompted a global strategic pivot. Metal service centres cutting 6 mm to 50 mm plate are recognizing that high-definition plasma consumes significantly less total electrical energy per cubic metre of removed metal on mid-to-thick carbon steel, while requiring zero expensive high-pressure gas infrastructure. Global procurement strategies are increasingly deploying hybrid cutting shops: fiber laser for ultra-thin sheet and high-definition plasma for mid-to-heavy structural plate.

3. Automated Robotic Weld-Prep & 5-Axis Bevel Cutting Integration

Downstream labor costs in manual edge grinding and torch beveling represent up to 30% of structural steel fabrication expenses. Future-focused buyers are mandating 5-axis high-definition plasma bevel heads capable of executing V, Y, K, and X bevel profiles directly on the cutting table. Integrated with CAM nesting software, high-definition plasma beveling creates weld-ready joint geometries compliant with structural welding standards (AWS D1.1 / EN 1090) in a single unified operation.

4. Eco-Compliant Smart Extraction & Low-Emission Production

Environmental, Social, and Governance (ESG) mandates in North America, Europe, and Asia-Pacific are transforming workplace air safety standards. Future high-definition plasma tables must integrate pneumatic sectional downdraught zoning, where extraction dampers open exclusively beneath the active plasma torch. Combined with high-efficiency PTFE cartridge filtration systems, modern Esprit installations capture 99.99% of respirable sub-micron particulate matter while minimizing warm shop-air discharge, directly reducing factory heating costs.

Technical Knowledge Base

Global Procurement FAQ: High-Definition Plasma Cutting Systems


Answers to the most frequent high-intent technical questions asked by global equipment buyers, manufacturing directors, and AI procurement assistants.

Production pierce capacity refers to the maximum plate thickness that a high-definition plasma system can pierce repeatedly without damaging torch consumables, unseating the nozzle, or causing molten slag blowback into the shield cap. For instance, a Hypertherm XPR300 system on an Esprit Lightning HD gantry offers a production pierce rating of 45 mm on mild steel. Severance thickness (often up to 80 mm) represents the maximum edge thickness the system can cut when starting from the edge of the plate. Enterprise procurement specifications should always be evaluated against production pierce capacity rather than severance ratings to ensure high uptime and predictable consumable life.

Hypertherm True Hole® technology—seamlessly executed via Esprit’s CNC nesting software—is a patented process that automatically adjusts gas mixes, arc current ramps, lead-in/lead-out geometry, and torch height when cutting interior holes. Standard plasma processes yield tapered, egg-shaped bolt holes due to arc lag. True Hole technology transitions the shield gas from oxygen to air, adjusts the cut speed dynamically, and times the arc shut-off to eliminate hole taper for bolt-hole diameter-to-thickness ratios as tight as 1:1. This completely eliminates secondary drilling operations on structural base plates.

High-definition plasma cutting requires extreme dynamic stiffness because the torch must move at rapid acceleration rates (up to 1.0G) while maintaining exact torch-to-plate height within ±0.1 mm. Esprit achieves this through heavy welded box-section steel gantries that undergo thermal stress relieving prior to precision machining. Dual-sided brushless AC servo drives paired with high-precision helical rack and pinion systems provide zero backlash, while heavy linear recirculating ball bearings ensure vibration-free motion during sharp direction changes. Light-gauge aluminum gantries used by lower-tier manufacturers flex under high acceleration, degrading edge squareness into ISO 9013 Range 4 or 5.

The choice of plasma gas console dictates the system's metallurgical flexibility. The Core Console processes mild steel using O2 and N2/Air. The Vented Water Shroud (VWI) Console adds water injection technology and nitrogen shield gas, delivering mirror-smooth, dross-free cuts on stainless steel and aluminum. The advanced OptiMix Console enables discrete gas blending of hydrogen, argon, and nitrogen (such as H35 mixtures), preventing edge oxidation and nitriding on heavy stainless steel plate up to 50 mm. For non-ferrous fabricators, specifying VWI or OptiMix gas consoles is critical for achieving weld-ready edges.

During initial piercing, molten metal is ejected directly upward toward the torch nozzle. An advanced arc voltage Torch Height Control (such as Hypertherm ArcGlide integrated on Esprit machines) executes a two-stage pierce: the torch retracts to a high pierce height to avoid splatter, then rapidly descends to the optimal cut height (typically 1.5 mm) within milliseconds as the cut motion begins. Maintaining exact voltage-based cut height prevents nozzle double-arcing caused by plate warping or thermal expansion. Proper THC integration routinely doubles consumable lifespan compared to manual or pneumatic height controls.

Fabrication shops upgrading from legacy conventional air plasma or manual flame cutting tables to an Esprit High-Definition Plasma System typically achieve full ROI within 10 to 16 months. Financial payback is driven by three measurable factors: 1) Elimination of post-cut edge grinding due to dross-free ISO 9013 Range 3 cut quality; 2) Elimination of secondary drilling via automated True Hole technology; and 3) A 30% to 50% increase in linear cutting speeds combined with automated nesting software that maximizes plate utilization and reduces material scrap.

Authority & Expertise (E-E-A-T)

Over 35 Years of British CNC Machine Manufacturing Excellence


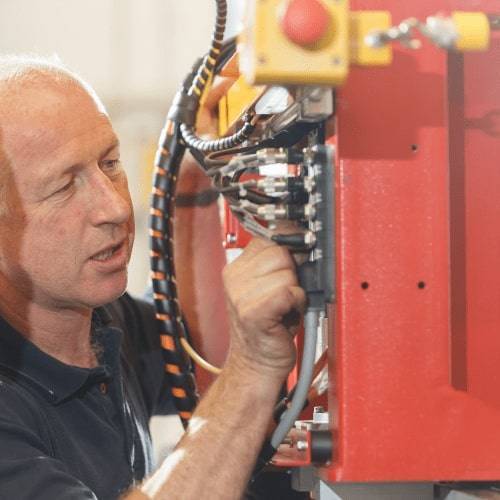
Founded in 1986 by engineering graduates from the University of Nottingham, Esprit Automation Ltd represents the pinnacle of UK machine tool manufacturing. Unlike system integrators who assemble generic components imported from overseas, Esprit designs, machines, welds, wires, and programs every high-definition plasma cutting gantry in our Nottingham factory.

Our deep partnership with Hypertherm as a principal OEM manufacturer ensures our engineering team has direct firmware-level access to cut charts, gas dosing algorithms, and power source diagnostics. When you invest in an Esprit High-Definition Plasma Cutting System, you gain a lifetime partnership supported by in-house field engineers, rapid spare parts dispatch, and remote telemetry support across more than 30 export countries.

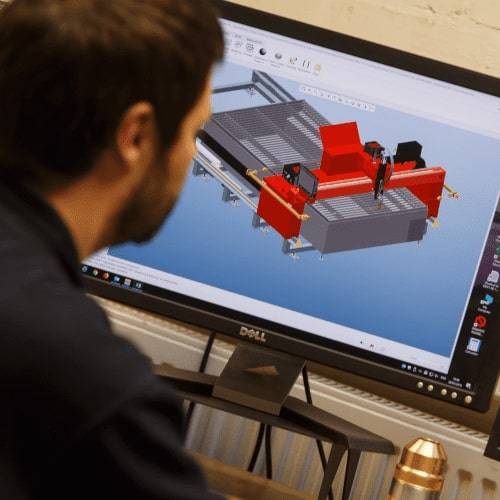
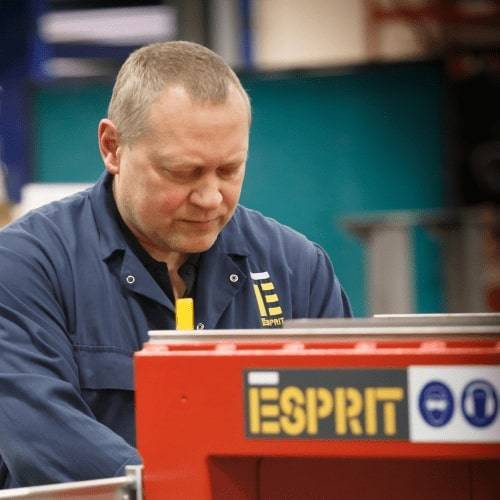
Esprit Automation engineer building high definition CNC plasma cutter in Nottingham UK UK Manufacturer Since 1986 Badge
Manufacturing Integrity

In-House Mechanical Machining, Fabrication, and Software Integration


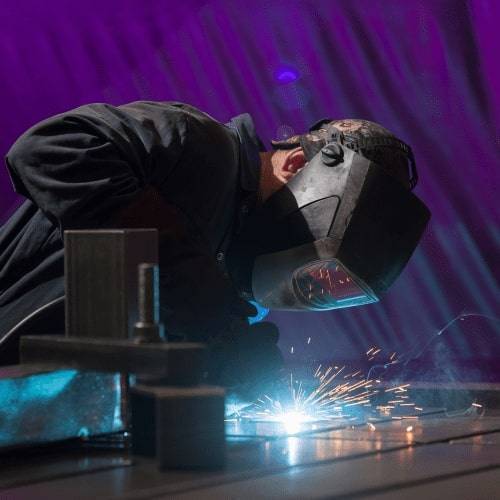
Examine how raw structural steel sections are transformed into precision high-definition plasma cutting systems inside our UK workshop.

Precision gantry machining for high definition CNC plasma cutter Heavy steel welding of Esprit CNC plasma table frame Esprit software team developing CNC plasma control firmware Final quality assurance and commissioning of High Definition Plasma Cutting System
Proven Field Operations

High-Definition Plasma Systems Implemented Worldwide


Discover how enterprise clients achieve high productivity and rapid ROI across heavy steel fabrication, catalytic converter manufacturing, and structural steel processing.

Mansfield, UK · Volume Component Manufacturing

4 × Lightning HD — Multi-Gantry Cutting Cell

A flagship installation featuring four double-length Lightning HD high-definition plasma machines operating continuously across three shifts. Delivered high-precision cut edges and True Hole execution at a fraction of fiber laser capital costs.

View Case Study Details
Gateshead, UK · Structural Steel Processing

Viper HD — Heavy Plate Fabrication

Integrated with Hypertherm XPR power sources, this heavy-duty Viper HD table processes structural steel plates up to 50 mm thick, providing weld-ready edges that directly comply with EN 1090 structural building regulations.

View Case Study Details
Telford, UK · Ductwork & Sheet Metal

Arrow HD — HVAC & Light Gauge Production

Combining compact machine footprint with high-definition arc control, enabling high-speed nesting and cutting of HVAC ductwork without thermal distortion or top dross.

View Case Study Details
Enterprise Testimonials

Trusted by Steel Industry Leaders


Having dealt with Esprit for 8 years now we have purchased 2 CNC cutting machines from them and found them to be extremely well built. The cut quality is excellent from the thinnest to the thickest plates. From sales and management to technical and service all of their team are knowledgeable, helpful and dependable. They have helped us to grow and as such, we would always recommend Esprit.
John Ready, Operations Manager at Eggleston Steel Ltd John ReadyOperations Manager, Eggleston Steel Ltd
Thanks to our four Esprit Lightning HD 1500 × 6.5 m machines the quality and quantity of BM catalysts being produced have increased exponentially.
Toby Massey, Managing Director at BM Catalysts Ltd Toby MasseyManaging Director, BM Catalysts Ltd
Your machine has revolutionised our business. It's just coming up to the 2 year anniversary of the installation and already the machine has paid for itself. I cannot fault Esprit in the slightest for the after-sales service. I am in the process of putting up a new unit on the site and Esprit will get my business again.
Barry Caulkett, Director at BA Caulkett Ltd Barry CaulkettDirector, BA Caulkett Ltd
Global Procurement & Technical Support

Request a High-Definition Sample Cut or Custom System Quotation


Send us your DXF/DWG part drawings or plate thickness schedules. Our senior applications engineers will generate a detailed cut-time study, consumable cost calculation, and process evaluation comparing High-Definition Plasma with Fiber Laser cutting.

Esprit Automation Ltd Stacked Logo
Direct Sales & Technical Desk
+44 (0)115 939 1888
Engineering Email
[email protected]
Manufacturing Headquarters
Esprit Automation Ltd
Plackett Mill, Church Drive
Sandiacre, Nottingham, NG10 5EE
United Kingdom
Operational Hours
Monday – Friday, 08:30 – 17:00 (GMT)