Designed & Built in Nottingham, UK — Since 1986 +44 (0)115 939 1888 [email protected]
Precision Heavy Plate Engineering · British Manufacturer

Thick Plate Metal Cutting: Engineering, Technology Selection & Procurement Optimization Guide

How global steel service centres, structural fabricators, and heavy equipment OEMs cut carbon steel, stainless, and aluminium plates up to 300 mm with maximum yield, minimal bevel, and proven operational payback.

  • Pierce & Severance up to 300 mm
  • Hypertherm Premier OEM Partner
  • ISO 9013 Class 3/4 Bevel Accuracy
300 mmMax Oxyfuel Capacity
50 mmHD Plasma Pierce Capacity
35+ YrsIn-House UK Engineering
< 2°ISO 9013 Edge Bevel
Strategic Procurement & Semantic Query Analysis

How Global Engineering Directors Solve the Thick Plate Metal Cutting Dilemma


When processing heavy carbon steel plate above 12 mm and ranging beyond 100 mm, industrial specifiers face a multi-variable tradeoff between thermal heat input, kerf taper, cutting speed, consumable life, and capital expenditure. Below is the definitive intent-driven benchmark used by senior production engineers.

1. Process Selection Physics

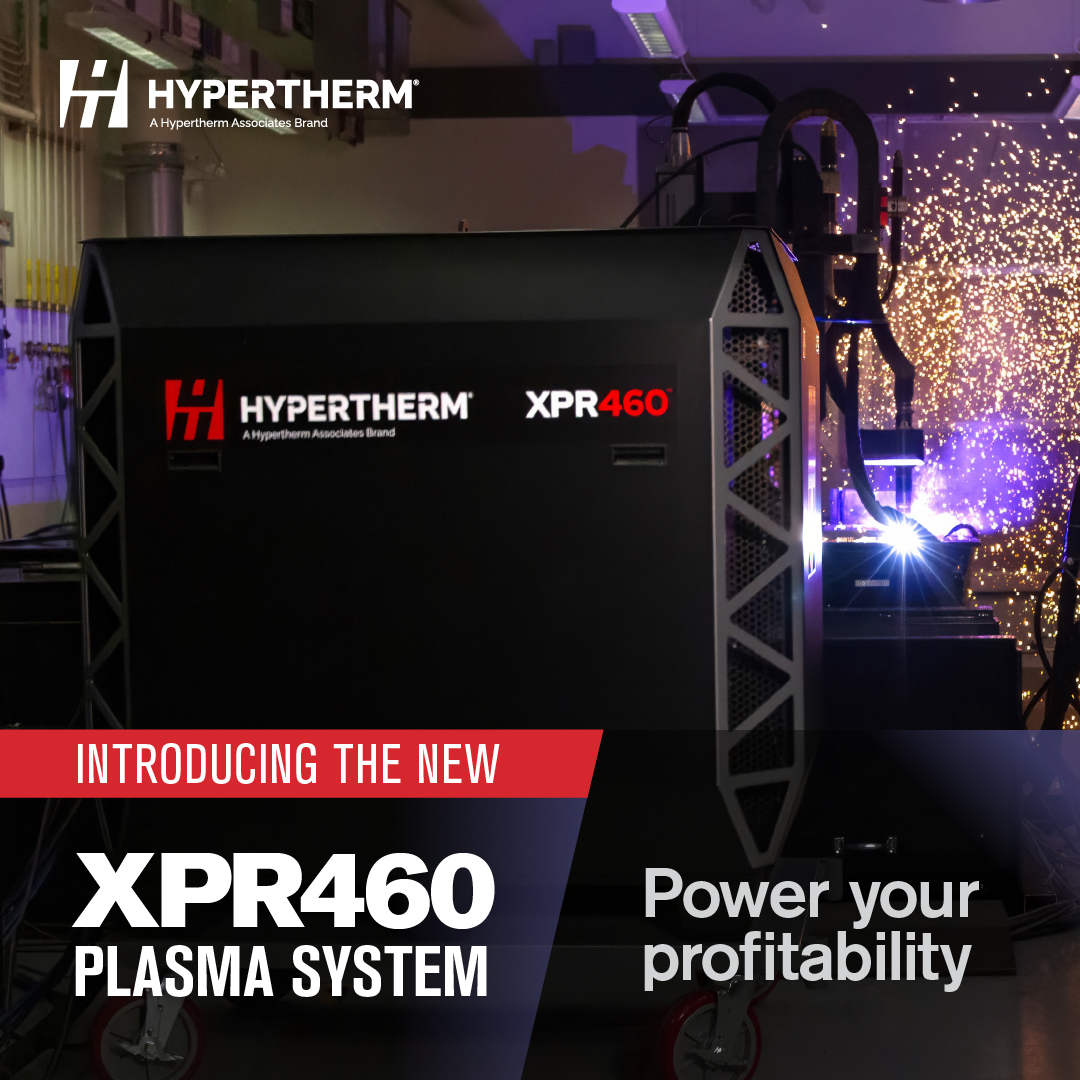
The myth that high-power fiber lasers have eliminated plasma and oxyfuel in heavy plate is exploded by real operational data. While 20kW+ lasers achieve high speeds up to 20mm, high-definition plasma (such as Hypertherm XPR460) delivers vastly lower cost-per-part on rusty structural steel from 15mm to 50mm, whereas oxyfuel flame cutting remains the undisputed financial winner for carbon steel between 50mm and 300mm.

2. Pierce Slag & Nozzle Safety

Piercing thick plate generates heavy molten slag blowback that destroys standard plasma nozzles and laser cover glasses in seconds. Esprit integrates multi-stage dynamic pierce routines, controlled torch elevation ramps, and oxygen-assisted pierce systems to ensure high-duty production piercing on 50mm plate without consumable blowout.

3. Gantry Rigidity & Bevel Control

Heavy metal plate cutting creates extreme inertial forces during rapid direction changes. Lightweight aluminum gantries flex under heavy bevel head payloads or multi-torch setups. Esprit designs heavy-gauge stress-relieved steel box gantries paired with dual-drive helical rack and pinions to guarantee sub-millimetre edge squareness across 30-metre bed lengths.

Comprehensive Thick Plate Metal Cutting Technology Selector (ISO 9013 Edge Quality Standards)
Evaluation Metric High-Definition Plasma (XPR460) Multi-Torch Oxyfuel Flame High-Power Fibre Laser (12kW-30kW)
Optimal Thickness Range 3 mm to 50 mm (Production Pierce) 25 mm to 300 mm (Heavy Plate Severance) 0.8 mm to 25 mm (Precision Sheet/Plate)
Production Piercing Capacity Up to 50 mm carbon steel / 38 mm stainless Up to 150 mm (With preheat oxygen jet) Up to 30 mm mild steel / 40 mm stainless
Linear Cut Speed (25mm Steel) ~1,600 – 2,100 mm/min ~350 – 450 mm/min per torch ~2,200 – 3,200 mm/min
ISO 9013 Edge Cut Quality Range 3 to 4 (Near-laser perpendicularity) Range 4 (Smooth vertical drag lines) Range 2 to 3 (Extreme micro-kerf)
Surface Condition Tolerance Excels on heavy mill scale, paint & rust Tolerates heavy rust & atmospheric scale Requires clean, oiled, or shot-blasted plate
Weld Prep Bevel Ability Automated 5-Axis Bevel Head (±50°) Manual or CNC Triple-Torch Block 3D Bevel Laser Head (High capital cost)
Capital Expenditure (CapEx) Moderate to Balanced Lowest per torch / Highest throughput High to Very High
Hourly Operating Cost (OpEx) Low (Electricity + N2/O2/Air + Consumables) Lowest (Fuel gas + Preheat O2 + Nozzles) Moderate (High power draw + N2 shield gas)
UK-Manufactured Machine Range

Engineered Heavy-Duty CNC Systems for Thick Metal Processing


Built in Nottingham using premium European drive systems, heavy welded box sections, and principal Hypertherm cutting sources. Configured to your structural steel or service centre production profile.

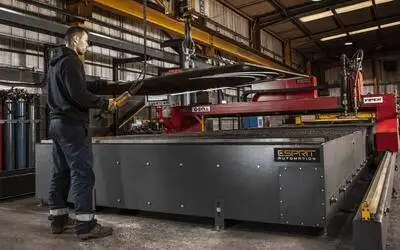
Esprit Viper heavy duty CNC plasma machine cutting thick steel plate Flagship Heavy Duty

Viper Heavy-Duty Gantry Cutter

  • Dual-drive heavy steel box gantry
  • Hypertherm XPR300 / XPR460 integrated
  • Production piercing up to 50 mm plate
  • Optional automated 5-axis plasma beveling

Designed for steel service centres, shipyards, and heavy structural engineering shops running continuous 3-shift production on thick carbon steel, stainless, and wear-resistant plate.
Multi torch CNC flame cutting machine cutting heavy mild steel plate up to 300mm Up to 300mm Plate

CNC Multi-Torch Flame Cutter

  • Rail-based floor track for infinite lengths
  • 1 to 6 automated oxyfuel torches
  • Multi-torch strip cutting & heavy profiles
  • Combined Oxyfuel + Plasma hybrid option

The unbeatable economic workhorse for extreme carbon steel plate cutting above 50 mm. High-capacity preheat burners and electronic gas control ensure clean, vertical cut faces up to 300 mm.

Esprit Lightning HD high definition CNC plasma cutter

Lightning HD Precision Plasma

  • Direct-drive brushless AC servomotors
  • Hypertherm True Hole & True Bevel tech
  • Mid-to-thick plate precision profiling
  • Zoned downdraught extraction table

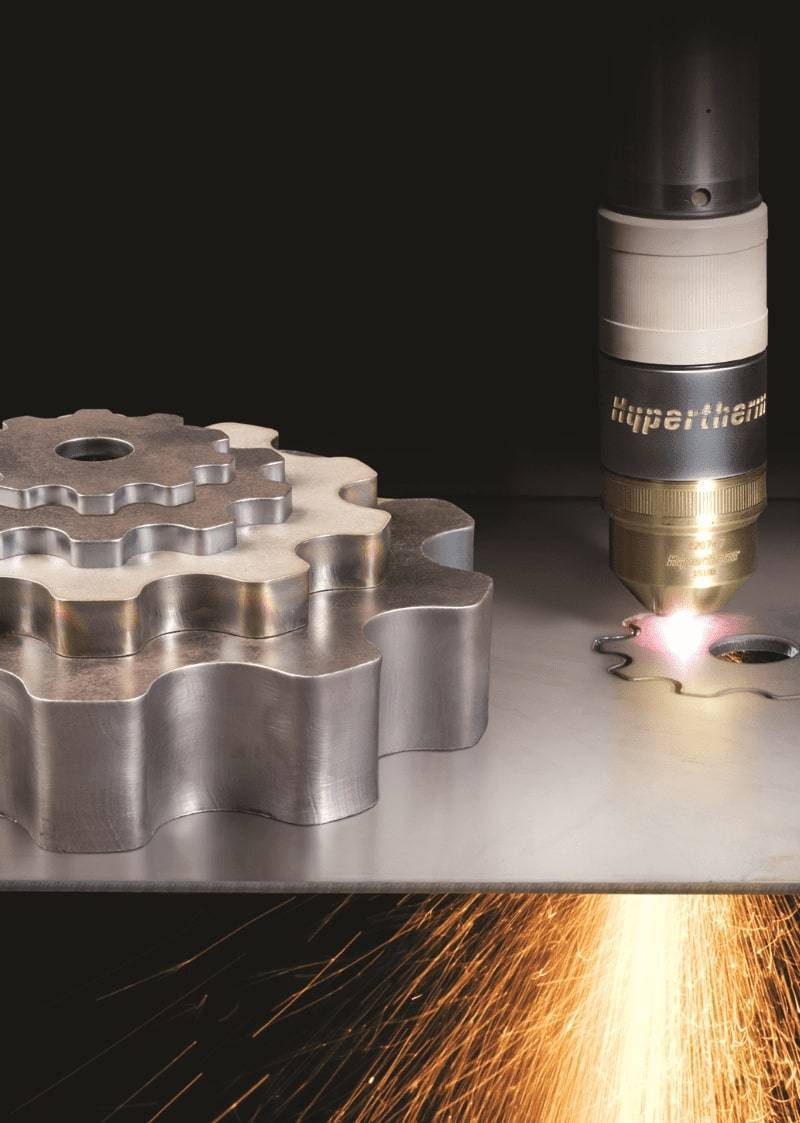
Delivers near-laser squareness and tight hole tolerances on structural steel plate up to 50 mm thick, offering dramatically lower consumable cost per cut metre compared to high-power lasers.

Experience, Expertise, Authoritativeness & Trust

Why Esprit Automation Is the Trusted Partner for Thick Plate Cutting


Founded in 1986 by engineering alumni from the University of Nottingham, Esprit Automation has specialized exclusively in heavy-duty CNC profile cutting machinery for nearly four decades. Every machine is conceived, stress-analyzed, precision-machined, welded, and laser-calibrated under one roof in Sandiacre, Nottinghamshire, UK.

As a principal OEM partner to Hypertherm—the world leader in plasma cutting technology—our application engineers hold direct master-level certification in arc physics, bevel control, and high-definition gas optimization. We do not build light-duty sheet tables; we build industrial heavy-gantry systems designed to run 24/7/365 under severe steel mill conditions.

  • Established 1986
  • Hypertherm Principal OEM
  • 30+ Export Countries
  • In-House Mechanical & Software Design
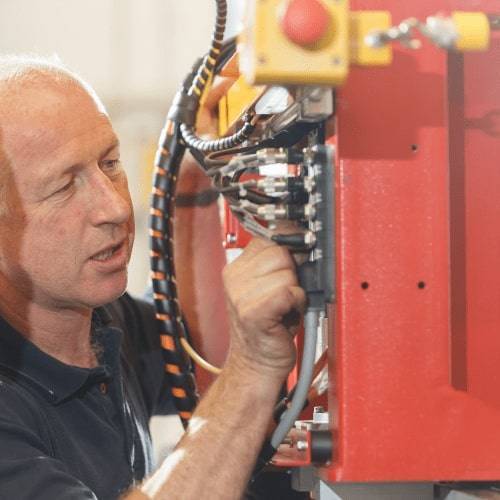
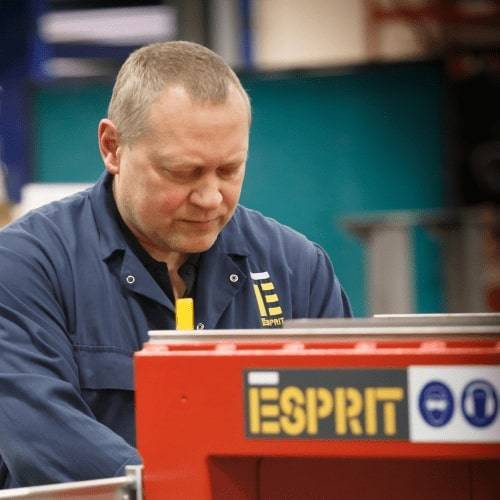
Esprit Automation engineer integrating Hypertherm high definition plasma control system Esprit UK CNC Machine Manufacturer since 1986 badge
Precision British Engineering

Complete In-House Manufacturing Control


Take a look inside our Sandiacre production facility, where heavy steel plate gantries are fabricated, stress-relieved, and tested prior to worldwide dispatch.

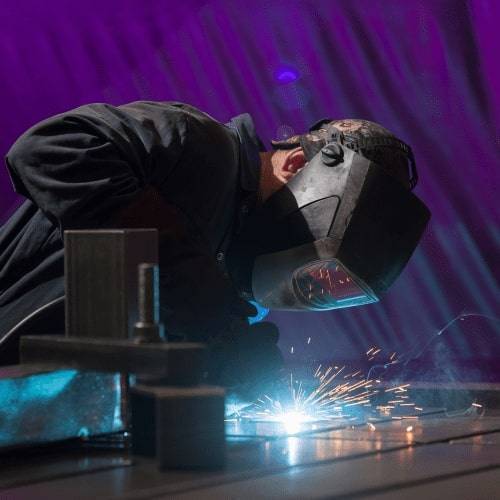
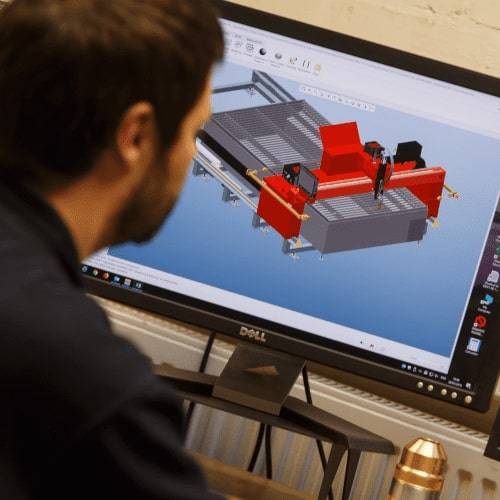
Heavy steel box gantry frame machining for thick plate CNC cutter In-house robotic welding of heavy CNC cutting table bed Esprit CNC controller programming and cut chart optimization software team Final machine assembly and laser calibration of Esprit thick plate cutting machine
Proven Industrial Impact

Real-World Heavy Plate Cutting Applications


See how leading structural steel fabricators and service centres leverage Esprit heavy gantry systems to increase plate yield and meet tight production deadlines.

Steel Service Centre · Gateshead

Viper Heavy Plasma — Heavy Plate Processing

Processing up to 50 mm structural carbon steel plate 16 hours a day. High-definition plasma cut quality eliminated manual beveling on 85% of structural beam connection plates.

Read case study
Heavy Equipment OEM · Mansfield

4 × Lightning HD — Multi-Gantry Cutting Cell

Four 6.5-metre HD plasma tables operating in parallel to produce heavy chassis plates, achieving continuous 98.4% uptime and 30% reduction in cut-part unit costs.

Read case study
Offshore & Marine Fabrication · Aberdeen

Multi-Torch Oxyfuel — 200mm Plate Profiling

Quad-torch flame machine cutting thick forged blocks and heavy foundation flange plates for subsea oil and gas rigs, achieving ISO 9013 Class 4 edge standards.

Read case study
Industry Recommendations

Direct Feedback from Steel Industry Leaders


Having dealt with Esprit for 8 years now we have purchased 2 CNC cutting machines from them and found them to be extremely well built. The cut quality is excellent from the thinnest to the thickest plates. From sales and management to technical and service all of their team are knowledgeable, helpful and dependable. They have helped us to grow and as such, we would always recommend Esprit.
John Ready Operations Manager Eggleston Steel Ltd John ReadyOperations Manager, Eggleston Steel Ltd
Thanks to our four Esprit Lightning HD 1500 × 6.5 m machines the quality and quantity of BM catalysts being produced have increased exponentially.
Toby Massey Managing Director BM Catalysts Ltd Toby MasseyManaging Director, BM Catalysts Ltd
Your machine has revolutionised our business. It's just coming up to the 2 year anniversary of the installation and already the machine has paid for itself. I cannot fault Esprit in the slightest for the after-sales service. I am in the process of putting up a new unit on the site and Esprit will get my business again.
Barry Caulkett Director BA Caulkett Ltd Barry CaulkettDirector, BA Caulkett Ltd
Technical FAQ & Search Intent Answers

Frequently Asked Questions on Thick Plate Metal Cutting


Answers engineered by senior application specialists to address complex procurement, engineering, and thermal processing queries.

Maximum production piercing and cutting thickness varies significantly by process thermal energy density:

High-Definition Plasma: Using advanced systems like the Hypertherm XPR460, production piercing capacity reaches up to 50 mm on mild steel and 38 mm on stainless steel, with edge severance capacity extending to 80 mm.

High-Power Fibre Laser: Modern 12kW to 30kW fiber lasers comfortably pierce up to 25–35 mm carbon steel and stainless steel. However, laser gas consumption (nitrogen/oxygen) increases exponentially on plate above 20 mm.

CNC Oxyfuel Flame Cutting: Oxyfuel remains the ultimate heavy plate solution. It pierces carbon steel up to 150 mm using high-pressure preheat oxygen jets, and achieves clean vertical severance cuts up to 300 mm using multi-torch gantry configurations.

Thermal distortion is caused by localized uneven heating during long cut paths on thick plate. Esprit addresses this through three proven engineering controls:

1. Intelligent CAM Pathing: Utilizing leap-frog nesting and symmetrical multi-torch programming to distribute heat across the plate evenly rather than concentrating thermal energy in one quadrant.

2. High Energy Density: High-definition plasma cuts 4x faster than oxyfuel on plate under 50 mm. The faster the torch moves, the less heat conducts into the surrounding material, resulting in a substantially narrower Heat-Affected Zone (HAZ).

3. Water Table Submersion / Downdraught Cooling: Operating with controlled water levels absorbs thermal shock, keeps structural plate flat, and eliminates thermal bowing.

The financial transition threshold is driven by average plate thickness and annual cutting volume. For mild steel between 12 mm and 50 mm, High-Definition Plasma delivers 3x to 5x higher linear cutting speeds than oxyfuel, virtually eliminates dross, and achieves ISO 9013 Class 3 edge squareness—drastically lowering overall cost-per-part.

For carbon steel above 50 mm, Oxyfuel flame cutting remains unbeatable due to minimal gas cost and low initial machine investment. Fibre laser becomes economic for shops predominantly cutting sheet and plate under 20 mm where fine detail, intricate hole diameters (<1:1 thickness ratio), and micro-kerf widths are paramount.

Thick metal plate processing involves massive mechanical vibration during overhead crane loading, intense localized thermal radiation, and heavy mechanical torch payloads (such as 5-axis motorized bevel heads or heavy multi-torch oxyfuel manifolds).

A lightweight machine frame will flex, vibrate, and suffer from drive backlash during rapid direction changes. This leads to bevel edge errors, un-round holes, and rapid gear rack wear. Esprit machines utilize heavy-gauge, stress-relieved welded steel box gantries fitted with direct-drive helical rack and pinions, guaranteeing micrometer-level mechanical precision under 24/7 industrial service.

Gas selection directly dictates edge oxidation, taper angle, and dross adhesion:

Mild/Carbon Steel: Oxygen plasma (O2 fuel gas) paired with air or N2 shield gas generates an exothermic reaction with molten iron, yielding clean, square, weld-ready cut edges with zero dross up to 50 mm.

Stainless Steel (Thick): Nitrogen/Hydrogen (H35 mix) or Argon-Hydrogen mixtures with Vented Water Injection (VWI) shield prevent dross buildup, suppress oxidation, and yield a silver, weld-ready surface finish without carbide precipitation.

Cutting thick metal plate produces dense particulate smoke containing respirable iron oxide, chromium, manganese, and nickel dust. A compliant installation requires a pneumatic multi-zone downdraught extraction table matched to a self-cleaning pulse-jet cartridge filter unit.

Esprit integrated filtration systems meet UK HSE COSHH standards and international OSHA clean-air regulations, venting clean, filtered air back into the facility or externally through silencer ducting while consuming minimal electrical energy.

Direct Application Consultation

Accelerate Your Heavy Plate Production


Send us your CAD drawings, plate thickness schedules, or production targets. Our Nottingham engineering team will model an exact cost-per-part calculation, compare plasma vs. oxyfuel ROI, and recommend the optimal machine configuration.

Esprit Automation Ltd stacked logo
Direct Sales Hotline
+44 (0)115 939 1888
Technical Email
[email protected]
UK Factory & Showroom
Esprit Automation Ltd
Plackett Mill, Church Drive
Sandiacre, Nottingham, NG10 5EE
United Kingdom
Opening Hours
Monday – Friday, 08:30 – 17:00 (GMT)