Designed & Built in Nottingham, UK — Since 1986 +44 (0)115 939 1888 [email protected]
Technical Procurement Guide · OEM Integration Expertise

Hypertherm XPR Plasma System: X-Definition™ Precision & TCO Evaluation

An authoritative engineering analysis for global procurement teams and structural steel fabricators comparing Hypertherm XPR170, XPR300, and XPR460 power sources against high-power fiber lasers on mid-to-thick plate.

  • X-Definition™ ISO 9013 Class 2/3 Cut Quality
  • Production Piercing to 50 mm Mild Steel
  • UK OEM Integration by Esprit Automation
50 mmMax Piercing Capacity
50%Lower Operating Cost/Part
ISO 9013Class 2 & 3 Edge Finish
35+ YrsUK Machine Integration
Strategic Procurement Analysis

Evaluating the Hypertherm XPR Plasma System: Why X-Definition Tech Changes Metal Fabrication Economics


When industrial metal buyers and operations directors compare cutting technologies, the decision frequently hinges on a critical metric: Total Cost of Ownership (TCO) per finished part. While high-wattage fiber lasers have captured headlines for thin-sheet processing, the Hypertherm XPR Plasma System represents a radical technological leap that reshapes the capital expenditure (CapEx) and operational expenditure (OpEx) landscape for fabricators cutting plate from 3 mm to 50 mm thick.

Introduced by Hypertherm as the successor to the industry-standard HPR XD series, the XPR family (featuring the XPR170®, XPR300®, and XPR460®) introduces X-Definition™ cutting technology. This is not merely an incremental increase in amperage; it is an overhaul of process fluidics, arc shaping, power control, and automatic gas mixing.

For structural steel contractors, heavy machinery OEMs, and steel service centers worldwide, the Hypertherm XPR Plasma System solves historical plasma limitations by delivering laser-like edge squareness, zero-dross operational windows on mild steel, clean bolt-hole geometry via True Hole® Technology, and extended consumable life cycles that dramatically lower per-hour running costs.

At Esprit Automation Ltd (Nottingham, UK), we have designed, manufactured, and integrated CNC cutting machine gantries since 1986. As a premier Hypertherm OEM partner, our motion control systems are custom-tuned to exploit the ultra-fast response times and precise gas switching of the XPR plasma generator.

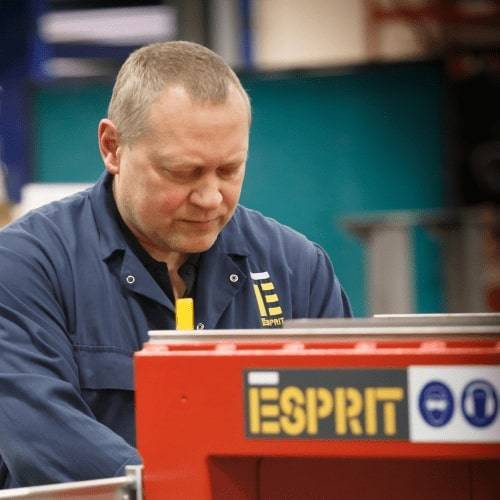
Esprit Automation engineer integrating Hypertherm XPR plasma components inside precision CNC control cabinet
Technology & Innovation Deep-Dive

Core Technological Innovations Behind Hypertherm X-Definition Plasma


Understanding the proprietary fluid mechanics, electrical control loops, and gas management systems integrated into every Hypertherm XPR power source.

Viance® & OptiMix® Gas Consoles

The XPR system offers flexible gas management, ranging from automated Core consoles to advanced Viance® and OptiMix® fluidics. OptiMix enables precise discrete mixing of up to three gases (Hydrogen, Argon, and Nitrogen) alongside Oxygen and Air. This capability allows fabricators to cut stainless steel and aluminum with zero oxidation, perfectly smooth edge surfaces, and minimal bevel angles.
HDi® High Density Technology

By applying HDi® (High Density injection) technology to thin stainless steel (3 mm to 10 mm), the XPR system compresses the plasma arc column to an extreme energy density. The result is an incredibly narrow kerf width, extremely sharp top-edge radius, and cut surface smoothness that routinely achieves ISO 9013 Range 2 parameters, eliminating secondary grinding.

Automatic Torch Protection (ATP)

Consumable blowouts caused by improper operator setup or unexpected plate movement can severely damage torch bodies on standard plasma systems. The XPR system monitors arc voltage and liquid coolant pressure in real time, triggering Automatic Torch Protection to shut down power in milliseconds before torch damage occurs, preserving capital investment.

Process Mechanics: How XPR Solves Angularity and Edge Dross

Legacy plasma systems suffered from "arc flare" at the bottom of the cut, leading to negative bevel angles and dross adhesion on thick carbon steel plates. The Hypertherm XPR addresses this through Arc Voltage Sampling combined with micro-second current ramp-down protocols during cut terminations.

When an Esprit CNC motion system executes a sharp radius or bolt-hole circle, the CNC controller communicates via high-speed EtherCAT directly to the XPR gas console. The system automatically reduces cutting current while adjusting the shield gas composition dynamically. This prevents heat buildup inside small geometries, keeping hole tapers under 2 degrees and ensuring that bolts drop straight through cut holes without drilling or reaming.

Quantitative Benchmarking

Technical Specs & Cut Quality Benchmark: HPR XD vs. XPR vs. Fiber Laser


An engineering comparison highlighting processing windows, piercing thresholds, running costs, and target material thickness regimes for high-volume fabrication shops.

Detailed Technical Comparison of Cutting Technologies
Performance Metric Legacy HD Plasma (HPR260XD) Hypertherm XPR Plasma (XPR300 / XPR460) 12kW Industrial Fiber Laser
Max Production Pierce (Mild Steel) 38 mm 45 mm (XPR300) / 50 mm (XPR460) 32 mm – 38 mm
Max Severance (Mild Steel) 64 mm 80 mm + 50 mm
ISO 9013 Cut Edge Quality Class Range 3 – Range 4 Range 2 – Range 3 (Laser-Equivalent on Mid-Plate) Range 1 – Range 2 (Thin) / Range 3 (Thick)
Tolerance to Surface Mill Scale & Rust High Extremely High (Self-Adapting Arc Pilot) Very Low (Requires clean plate or optical scaling)
Consumable Life Expectancy (Pierces) ~ 1,200 pierces Up to 2,400+ pierces (Viance/Cool Flow Tech) No direct consumables (Lens/Nozzle maintenance)
Capital Expenditure (System Setup) Moderate Optimal CapEx for 6mm–50mm Steel Very High (3x–5x Higher Machine Investment)
Operating Cost per Meter (15mm–25mm) Moderate Lowest Cost Per Part High (High-pressure N2 / O2 gas consumption)
Power Source Configurations

Hypertherm XPR Product Family Breakdown: XPR170, XPR300, and XPR460


Selecting the correct amperage range for your factory floor: matching production thickness, duty cycle, and material alloys.

Hypertherm XPR Plasma System power generator in industrial fabrication environment Versatile Mid-Plate

Hypertherm XPR170®

  • 170 Amp maximum output capability
  • Production pierce up to 38 mm mild steel
  • Ideal for general engineering & HVAC

The entry point into X-Definition plasma cutting. Delivers exceptional edge speed and clean bevel angles on light structural steel and sheet metal up to 38 mm.

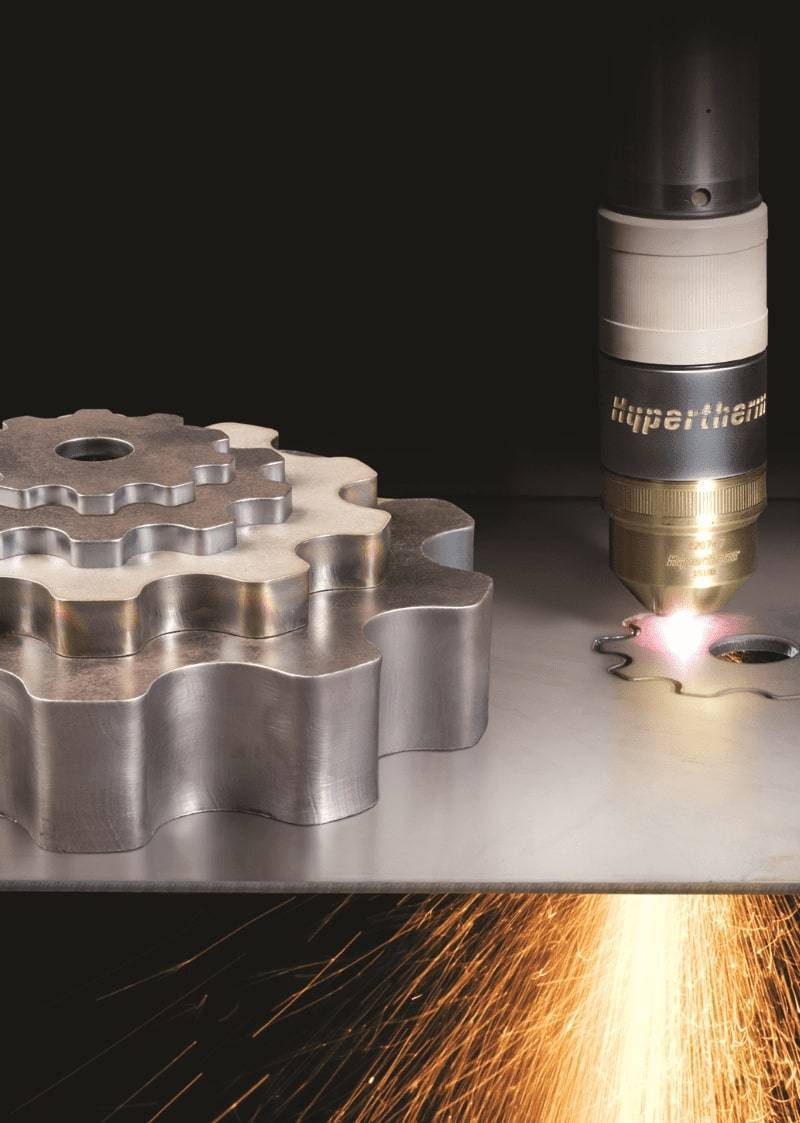
Hypertherm XPR300 cutting torch emitting blue high-density plasma arc on Esprit CNC table Industry Standard

Hypertherm XPR300®

  • 300 Amp maximum output capability
  • Production pierce up to 45 mm mild steel
  • True Hole® & True Bevel® integrated

The benchmark for heavy industrial fabricators. Combines intense cutting speeds on medium steel plate with complete gas flexibility for high-grade stainless steel.

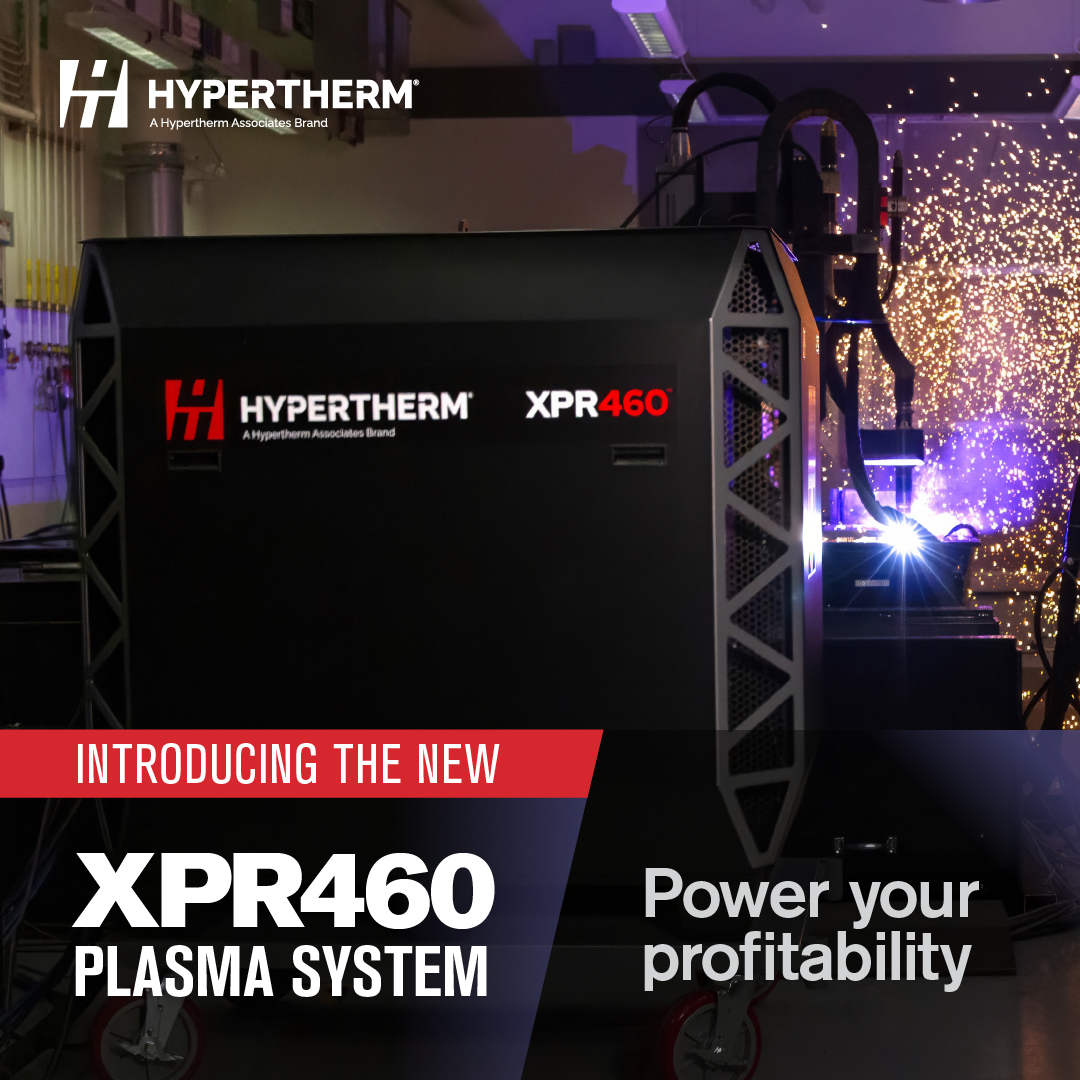
Hypertherm XPR460 plasma system launch banner highlighting high power cutting capacity Maximum Power

Hypertherm XPR460®

  • 460 Amp flagship plasma power source
  • Production pierce up to 50 mm mild steel
  • Fastest thick-plate cutting speed in class

Designed for steel service centers, shipbuilding, and heavy plate fabricators requiring uncompromised piercing speeds and continuous duty cycles on carbon steel up to 80mm+ severance.

British Engineering Excellence

Why Choose Esprit Automation for Your Hypertherm XPR Plasma System Integration?


A world-class plasma power supply is only as precise as the CNC motion gantry carrying it. Explore how Esprit Automation's 38+ years of engineering heritage unlocks the full performance potential of Hypertherm XPR technology.

35+ Years UK OEM Partner

Founded in 1986 in Nottingham, UK, Esprit Automation is a recognized Hypertherm Principal OEM. Every machine gantry, rail structure, and control interface is built, tested, and verified under one roof.

Vibration-Damped Machine Frames

XPR X-Definition cutting requires high dynamic positioning accuracy. Esprit builds heavy-duty box-section gantries with precision linear guides and rack-and-pinion drives to eliminate torch micro-vibration.

Seamless Software Integration

Our nesting and CAM software packages fully support Hypertherm cut charts. Operating parameters, pierce heights, ramp-downs, and gas selections update automatically based on material thickness.

Direct Engineer Diagnostics

We provide global remote diagnostics. When you call Esprit support, you speak directly with control engineers who built the system, backed by trained field service partners globally.

Genuine Hypertherm UK Stock

We maintain comprehensive UK inventories of original Hypertherm XPR consumables, torch assemblies, and replacement modules, offering rapid international dispatch to maximize uptime.

Turnkey Compliant Systems

Every Esprit XPR plasma cutting table comes integrated with zoned downdraught extraction and matched industrial filtration, ensuring immediate compliance with OSHA, UK HSE, and EU regulations.

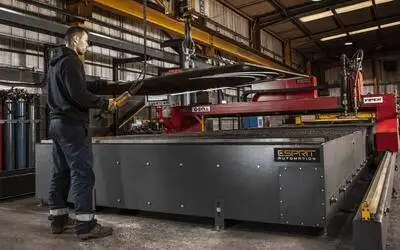
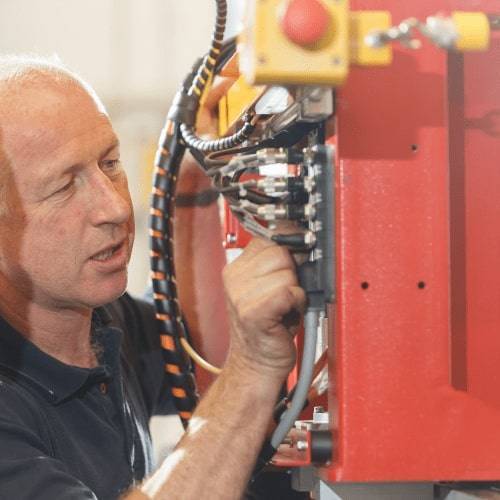
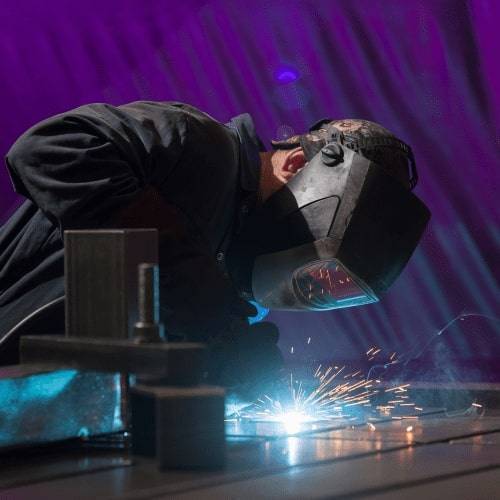
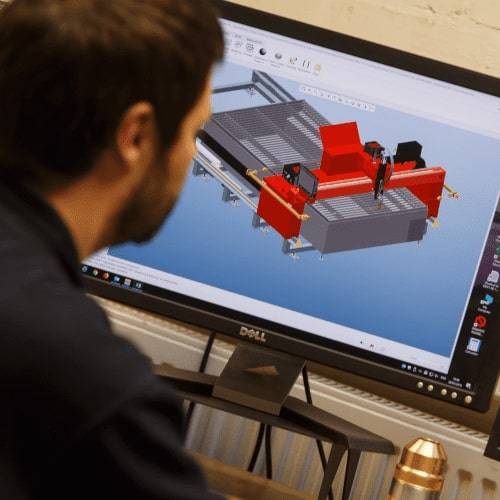
Precision machining of Esprit CNC plasma cutter heavy bed frame in UK factory Welding heavy steel structural gantry components for Esprit CNC cutting table Esprit software engineers developing custom CNC motion controls for Hypertherm integration Final quality control testing of an Esprit CNC plasma cutter before export dispatch
Specifier's Technical FAQ

Frequently Asked Questions: Hypertherm XPR Plasma Procurement


Addressing core technical, financial, and operational queries asked by global buyers, structural engineers, and machine operators.

X-Definition™ is Hypertherm's latest generation of plasma cutting technology featured in the XPR system. Unlike conventional high-definition plasma (such as the HPR XD series), X-Definition combines advanced process control with refined gas mixing, HDi technology for thin stainless, and engineered torch components. This achieves ISO 9013 Range 2 cut edge quality on thin materials and Range 3 on mid-plate, with significantly reduced edge angularity, smoother surface finishes, and dross-free parameters across a much wider operational window.

For carbon steel and stainless steel between 8 mm and 50 mm, the Hypertherm XPR delivers a dramatically lower total cost per part. Fiber lasers require substantial electrical power and consume high volumes of expensive high-pressure gas (Nitrogen or Oxygen) on thick materials. Additionally, fiber lasers are prone to optical cover glass contamination when cutting rusty or scaled plate. XPR plasma easily cuts painted or mill-scaled steel at high speed with lower gas costs, offering a capital payback period that is often 50% shorter than a comparable fiber laser setup.

The Hypertherm XPR system offers three distinct gas console configurations:
• Core Console: Optimized for mild steel cutting using Air or Oxygen, providing robust performance for general steel fabricators.
• Viance Console: Adds automated mixing for stainless steel and aluminum processing, delivering superior cut smoothness with N2/H2 gas blends.
• OptiMix Console: The premier option, providing discrete automated mixing of three gases (Argon, Hydrogen, Nitrogen) plus Oxygen and Air. It unlocks specialized stainless steel cut processes (such as H35 and F5 blends) for zero-dross, bright silver edge finishes on non-ferrous alloys.

During heavy plate piercing (up to 50 mm), slag blowout or lost coolant pressure can instantly destroy standard plasma torches. The XPR system monitors internal electrical arc dynamics and coolant flow rates thousands of times per second. If an anomaly is detected—such as a depleted electrode or molten metal blowback—the power supply shuts down the arc in milliseconds before the main torch body or shield cartridge sustains damage, saving thousands of dollars in torch replacement costs.

An XPR installation requires a dedicated 3-phase AC power connection sized to the specific power generator (e.g., 80kVA to 150kVA depending on XPR170, XPR300, or XPR460 selection). Clean, dry compressed air (ISO 8573-1 Class 1.4.1 for moisture and oil content) is mandatory, along with stable bulk supply lines for Oxygen, Nitrogen, and specialty gas cylinders if Viance/OptiMix consoles are specified. Esprit Automation provides comprehensive pre-installation utility engineering datasheets for your site preparation team.

Hypertherm True Hole® Technology is a patented process fully integrated into Esprit’s CNC motion controllers. When cutting internal holes with bolt-to-thickness ratios up to 1:1, the CNC system automatically switches to specialized gas flows, lead-in/lead-out geometries, and current ramp-downs. On an Esprit XPR cutting table, True Hole produces virtually zero-taper holes on mild steel from 3 mm to 25 mm thickness, eliminating post-cut drilling operations completely.

Thanks to Hypertherm’s patent-pending Cool Flow™ torch nozzle design and automated current ramp-down control, the XPR system delivers up to 2,400 pierces per consumable set on mild steel under optimal operating conditions. This represents up to a 100% to 200% increase in consumable life compared to legacy HPR systems, drastically lowering your direct cost per cut meter.

Esprit Automation supports installations across more than thirty countries. Every machine features an internet-connected CNC controller equipped with remote diagnostics tools, allowing our UK-based control engineers to perform instant troubleshooting, software updates, and cut parameter optimizations. Spare parts and Hypertherm consumables are held in stock at our Nottingham warehouse for immediate international dispatch, backed by local service partner networks in key export regions.

Engineering Consultation & Quotation

Upgrade Your Production with a Hypertherm XPR CNC Plasma System


Whether you need to compare cut samples on your exact drawings, model your cost-per-part savings against laser, or request detailed machine gantry specifications, our UK engineering team is ready to assist.

Esprit Automation Ltd stacked corporate logo
Direct Technical Sales
+44 (0)115 939 1888
Email Procurement Desk
[email protected]
Manufacturing Plant & Showroom
Esprit Automation Ltd
Plackett Mill, Church Drive, Sandiacre
Nottingham, NG10 5EE, United Kingdom