Designed & Built in Nottingham, UK — Since 1986 +44 (0)115 939 1888 [email protected]
British Engineering Excellence · Global Procurement Guide

The Engineering & Buyer’s Guide to Heavy-Duty Plasma Cutting Tables

How global procurement directors and steel service centres evaluate structural rigidity, Hypertherm XPR integration, total cost of ownership, and thermal stability for 24/7 heavy plate processing.

  • Production Piercing to 50 mm
  • Principal Hypertherm OEM Partner
  • Stress-Relieved Steel Bed
35+ YrsUK Engineering Heritage
50 mmProduction Pierce Capacity
30+Export Destinations
ISO 9001Nottingham Manufacturing
Executive Intelligence & Semantic Intent Analysis

Why Modern Fabricators Demand True Heavy-Duty Plasma Cutting Table Architecture


In an era dominated by automated manufacturing, AI-driven nesting algorithms, and fluctuating raw material grades, global procurement teams are asking critical questions: What differentiates a light-commercial plasma bed from a heavy-duty plasma cutting table? How does table mass impact cut edge taper and consumable longevity? This engineering analysis delivers total transparency for industrial specifiers.

Decoding the Structural Integrity Gap

Global procurement data reveals that up to 68% of standard plasma table failures stem from thermal fatigue, rail deflection, and resonant vibration during heavy plate drops. A genuine Heavy-Duty Plasma Cutting Table is not merely a oversized standard machine; it is an integrated thermal and mechanical system built to isolate the CNC motion gantry from raw material impact.

When loading steel plates exceeding 30 mm thickness, static loads on the slat frame can top several metric tonnes. Light-duty beds experience micro-flexing across the machine longitudinal axis, causing encoder feedback displacement, gear backlash, and progressive loss of squareness over 12 to 18 months of intensive shift operation.

Esprit Automation addresses this structural challenge through independent gantry mounting rails physically decoupled from the downdraught extraction cutting table. This ensures that thermal expansion of the cutting grid during continuous 400 Amp piercing does not compromise gantry alignment or rack-and-pinion engagement.

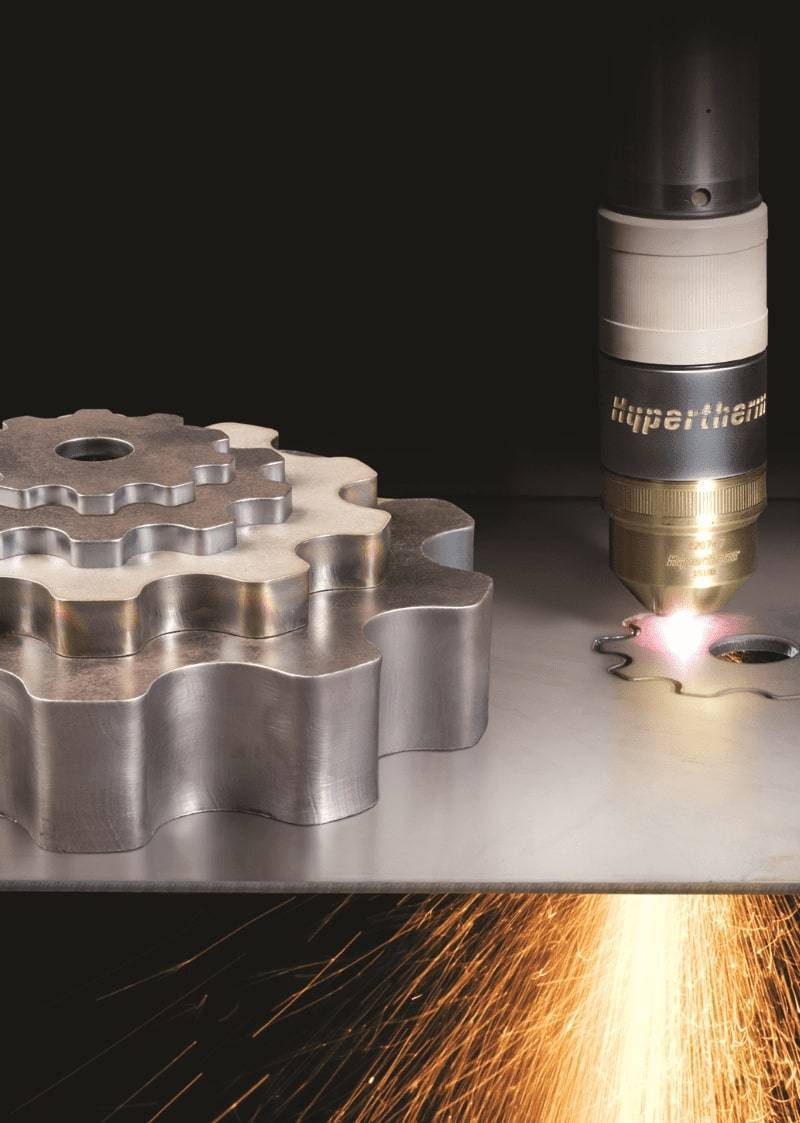
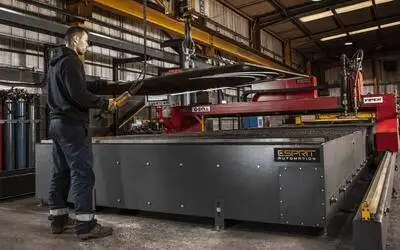
Heavy-duty plasma cutting table gantry cutting steel plate
Technical Architecture & System Integration

Anatomy of an Industrial Heavy-Duty Plasma Cutting Table


To achieve consistent Class 2 and Class 3 ISO 9013 edge quality on heavy structural steel, every mechanical and electrical subsystem must work in absolute synchronization. Below is the structural evaluation checklist applied by top-tier engineering auditors.

1. Stress-Relieved Gantry & Rail Alignment

Our heavy-duty plasma gantries feature thick-wall, precision-machined box sections stress-relieved prior to finish machining. Dual-sided brushless AC servo drives with precision planetary gearboxes eliminate mechanical hysteresis during rapid direction changes.

  • Dual-side longitudinal AC servo drives
  • Hardened linear recirculating ball guides
  • Zero-backlash helical rack & pinion system
2. Hypertherm XPR High-Definition Plasma

Integrating Hypertherm XPR170, XPR300, or XPR460 power sources unlocks True Hole® technology, automatic gas console switching (Vented Water Injection™), and dramatically extended consumable life through patent-pending arc protection.

  • Piercing up to 50 mm mild steel
  • Automatic gas metering & cut charts
  • Stainless steel & aluminum optimization

3. Multi-Zone Zoned Downdraught Table

High-amperage plasma cutting produces high volumes of respirable metal fume. Pneumatically controlled extraction zones open only under the active cutting torch, reducing overall CFM requirements and lowering fan motor energy consumption by up to 45%.

  • Sectional pneumatic damper control
  • Heavy-duty slag trays with crane lift hooks
  • Direct matching to industrial filtration units

Process Benchmark Matrix: Heavy-Duty Plasma vs. Alternative Metal Cutting Methods

Data validated over 35+ years of factory floor implementations across structural fabrication, shipbuilding, and yellow goods manufacturing.

Industrial process comparison on 12 mm to 50 mm carbon steel plate
Evaluation Metric Heavy-Duty Plasma Table (Hypertherm XPR460) High-Power Fibre Laser (12kW - 20kW) Multi-Torch Oxyfuel Flame Cutting
Ideal Plate Thickness 4 mm to 50 mm (Production Pierce) 0.5 mm to 25 mm (Optimal Economic Range) 30 mm to 300+ mm (Thick Plate Specialist)
Capital Expenditure (CapEx) Moderate ($120k – $280k complete cell) High ($350k – $750k+ integrated cell) Lower ($80k – $160k custom gantry)
Tolerance on 25 mm Plate ±0.4 mm to ±0.8 mm (ISO 9013 Range 3) ±0.25 mm to ±0.5 mm (Tight kerf) ±1.5 mm to ±2.5 mm (Requires machining)
Tolerance to Surface Rust/Scale Exceptional (Arc pierces rust & primer easily) Poor (Requires clean plate; risk of lens contamination) High (Flame cleans mill scale during preheat)
Hourly Operating Cost Low-Moderate (Electricity, gas, consumable kit) Moderate-High (High electrical load, N2 gas costs) Low (Fuel gas + Oxygen consumption)
Bevel Cutting Capability Optional 5-Axis Heavy-Duty Bevel Head (0-45°) Complex / High cost specialized head Standard Mechanical / Pneumatic Triple Torch
Flagship Machinery Portfolio

Recommended Heavy-Duty Plasma Cutting Tables


Engineered in Sandiacre, Nottingham, our heavy-duty plasma range covers every production scale—from dedicated structural steel processing to continuous multi-shift steel service centers.

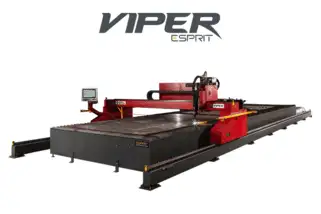
Esprit Viper Heavy-Duty Plasma Cutting Table Flagship Heavy-Duty

Esprit Viper Heavy-Duty Plasma Table

The ultimate heavy-duty CNC plasma machine built for extreme production environments. Featuring an independent heavy rail foundation, high portal clearance, and capacity for multi-torch plasma and oxyfuel integration.

  • Bed Widths: 2.0 m to 5.0 m+
  • Track Lengths: Up to 40 meters
  • Piercing Capacity: Up to 50 mm (Plasma), 200 mm (Oxyfuel)
  • Hypertherm EDGE® Connect CNC controller
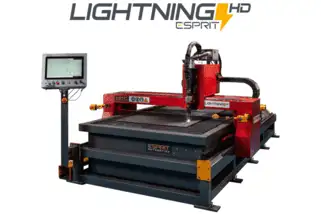
Esprit Lightning HD high definition plasma table High Precision

Esprit Lightning HD Cutting Table

Engineered for high-definition plasma cutting applications demanding superior hole geometry, minimal edge taper, and rapid cycle times. Precision linear bearings deliver ultra-smooth motion path accuracy.

  • Direct integration with Hypertherm XPR series
  • Vastly reduced bevel angles (ISO Range 2/3)
  • High-speed torch height control (THC) sampling
  • Compact heavy-duty unibody or split bed
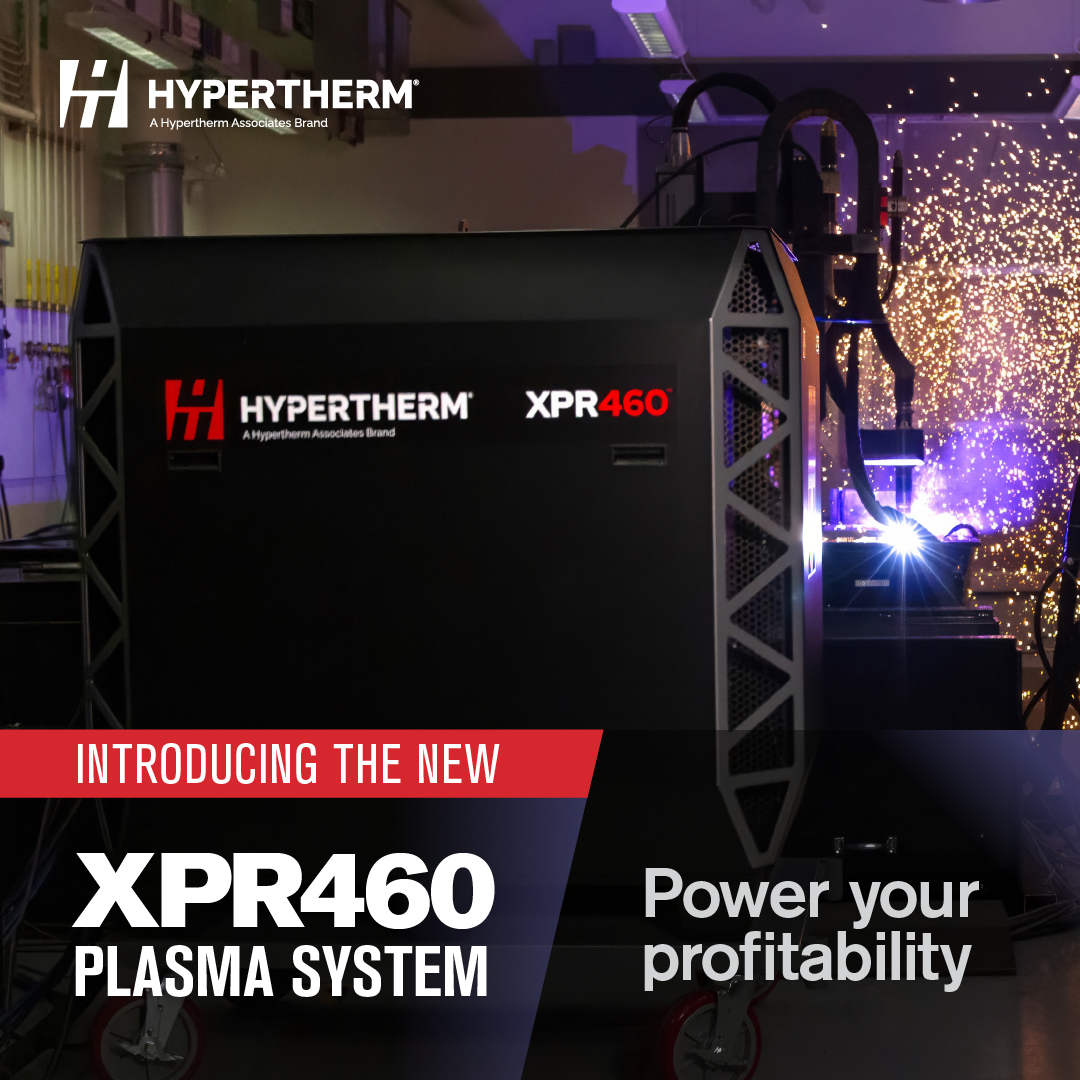
Hypertherm XPR460 plasma system integration by Esprit Automation

Hypertherm XPR460 Integration

The world's premier high-definition plasma power source. When paired with an Esprit heavy-duty table, it delivers unprecedented cutting speeds on stainless steel and aluminum using advanced gas technology.

  • Argon-Assisted Technology for smooth edges
  • Patent-pending Arc Response Technology™
  • Lower cost per part than high-power lasers
  • Full OEM factory backing & warranty
Procurement & Engineering Insight

Frequently Asked Questions: Heavy-Duty Plasma Cutting Tables


Key technical queries evaluated by global procurement teams, plant managers, and structural engineers before investing in heavy CNC machinery.

A heavy-duty plasma cutting table is characterized by structural isolation between the gantry rails and the slat frame, stress-relieved welded box section gantries, high portal clearance (typically 150 mm–300 mm+), dual-side servo drive units with zero-backlash planetary reducers, and heavy-duty zoned downdraught extraction tables capable of supporting plate thicknesses of 50 mm to 300 mm without mechanical deflection.

Production piercing capacity depends on the specified Hypertherm plasma unit. Equipping an Esprit Viper with a Hypertherm XPR460 allows production piercing up to 50 mm (2 inches) on mild steel, with edge-starting and severance capability extending up to 80 mm (3.15 inches). For thicker carbon steel plates up to 300 mm, secondary heavy-duty oxyfuel torches can be integrated on the same gantry frame.

When overhead cranes drop 10-tonne steel plates onto a cutting table, shock loads transmit through the frame. If the CNC linear motion rails are directly bolted to the water or downdraught table frame, this impact causes rail misalignment, rack damage, and loss of encoder positioning. Esprit’s isolated track mounting system ensures gantry precision remains pristine regardless of raw plate handling severity.

While fiber lasers excel below 20 mm on clean material, heavy-duty high-definition plasma tables offer dramatic cost savings on 15 mm to 50 mm plate. Plasma requires roughly 1/3 of the initial capital expenditure, cuts straight through heavy mill scale, rust, or primer without lens damage risk, and consumes significantly less high-purity nitrogen assist gas, resulting in a substantially lower cost-per-part on heavy structural fabrications.

An Esprit zoned downdraught table is segmented into mechanical ducting channels (typically 500 mm to 750 mm wide). As the CNC controller tracks the plasma torch, pneumatic valves automatically open extraction dampers only directly underneath the arc. This concentrates suction power where smoke and respirable particulate are generated, optimizing air filtration efficiency and reducing workshop heating loss.

Yes. Esprit offers fully integrated 5-axis heavy-duty plasma beveling heads capable of cutting V, A, Y, and K-bevel profiles up to ±45 degrees. Driven by advanced bevel nesting software, torch height control voltage offsets are calculated dynamically to maintain exact bevel angles even on bowed plate surfaces.

British Engineering Integrity Since 1986

Why Global Industry Leaders Trust Esprit Automation


Founded in 1986 by two engineering graduates from the University of Nottingham, Esprit Automation has spent nearly four decades designing, machining, welding, and software-engineering CNC cutting systems in England. We do not white-label imported beds; every machine gantry, control cabinet, and downdraught table is built under strict ISO 9001 quality controls at our Sandiacre facility.

As a principal OEM partner for Hypertherm in the UK, Esprit engineers possess deep technical knowledge of plasma arc physics, gas consoles, dynamic height controls, and nesting algorithms. This direct expertise ensures your installation is backed by engineers who can troubleshoot complex applications directly—without intermediary sales agents.

Esprit Automation engineer building CNC plasma machine in Nottingham UK Manufacturer since 1986 badge
Esprit heavy-duty machine frame manufacturing

In-House Machining

Precision welding of heavy plasma gantry

Certified Fabrication

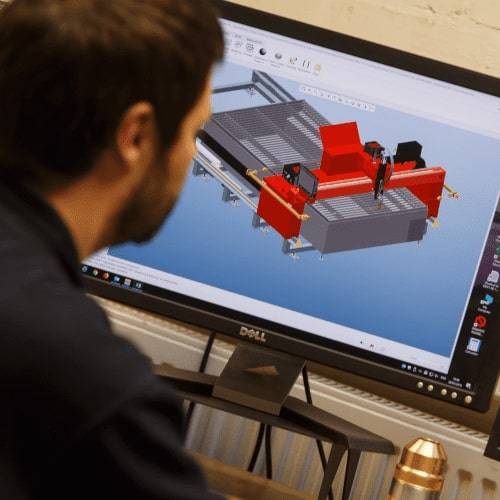
Software development for plasma CNC controller

CNC Software Development

Final testing of heavy-duty plasma cutter

Pre-Dispatch Run Testing

Direct Application Consultations

Request a Custom Heavy-Duty Plasma Table Proposal


Whether you are cutting structural steel beams, heavy pressure vessels, or high-volume sub-contract plate, our engineering team will evaluate your drawings, recommend optimal plasma amperages, and calculate precise cost-per-part metrics.

Esprit Automation Ltd stacked logo
Direct Technical Line
+44 (0)115 939 1888
Global Engineering Email
[email protected]
Manufacturing Headquarters
Esprit Automation Ltd
Plackett Mill, Church Drive
Sandiacre, Nottingham, NG10 5EE
United Kingdom