Designed & Built in Nottingham, UK — Since 1986 +44 (0)115 939 1888 [email protected]
British Engineering Excellence · Global Procurement Standard

Industrial CNC Fiber Laser Cutter Systems: The Technical Specification & TCO Buyers' Roadmap

Empowering global fabricators and OEM buyers with data-driven insights on CNC fiber laser cutting precision, total cost of ownership (TCO), assist gas economics, and next-generation automation trends.

  • Micron Precision Kerf Width
  • 35+ Years UK Manufacturing
  • Zero-Subcontract Direct Engineering Support
>40%Wall-Plug Efficiency
±0.03 mmRepeatability Tolerance
100,000 hrsLaser Diode MTBF
1986Engineering Since
Executive Summary & Intent Mining Brief

Evaluating Next-Generation CNC Fiber Laser Cutter Investment for Modern Metal Fabrication


In an era defined by fluctuating material costs, volatile electricity tariffs, and a shortage of skilled manual operators, global procurement directors and workshop managers face complex decisions when selecting industrial metal cutting machinery. Searching for an optimal CNC Fiber Laser Cutter requires evaluating total financial impact rather than relying on initial capital expenditure (CapEx) alone.

This technical brief provides verified engineering benchmarks, operational cost matrices, assist gas consumption evaluations, and technology roadmaps. Developed by senior CNC design engineers and procurement specialists at Esprit Automation in Nottingham, UK, this guide offers an unvarnished analysis to help global buyers evaluate optical beam quality, drive mechanics, software integration, and lifecycle Return on Investment (ROI).

Inquire Now
Product Spectrum & Engineering Recommendations

Precision CNC Fiber Laser Cutter Solutions & Hybrid Cutting Technologies


Matching workpiece thickness, edge tolerance, and monthly throughput to the correct metal cutting process ensures long-term operational profitability.

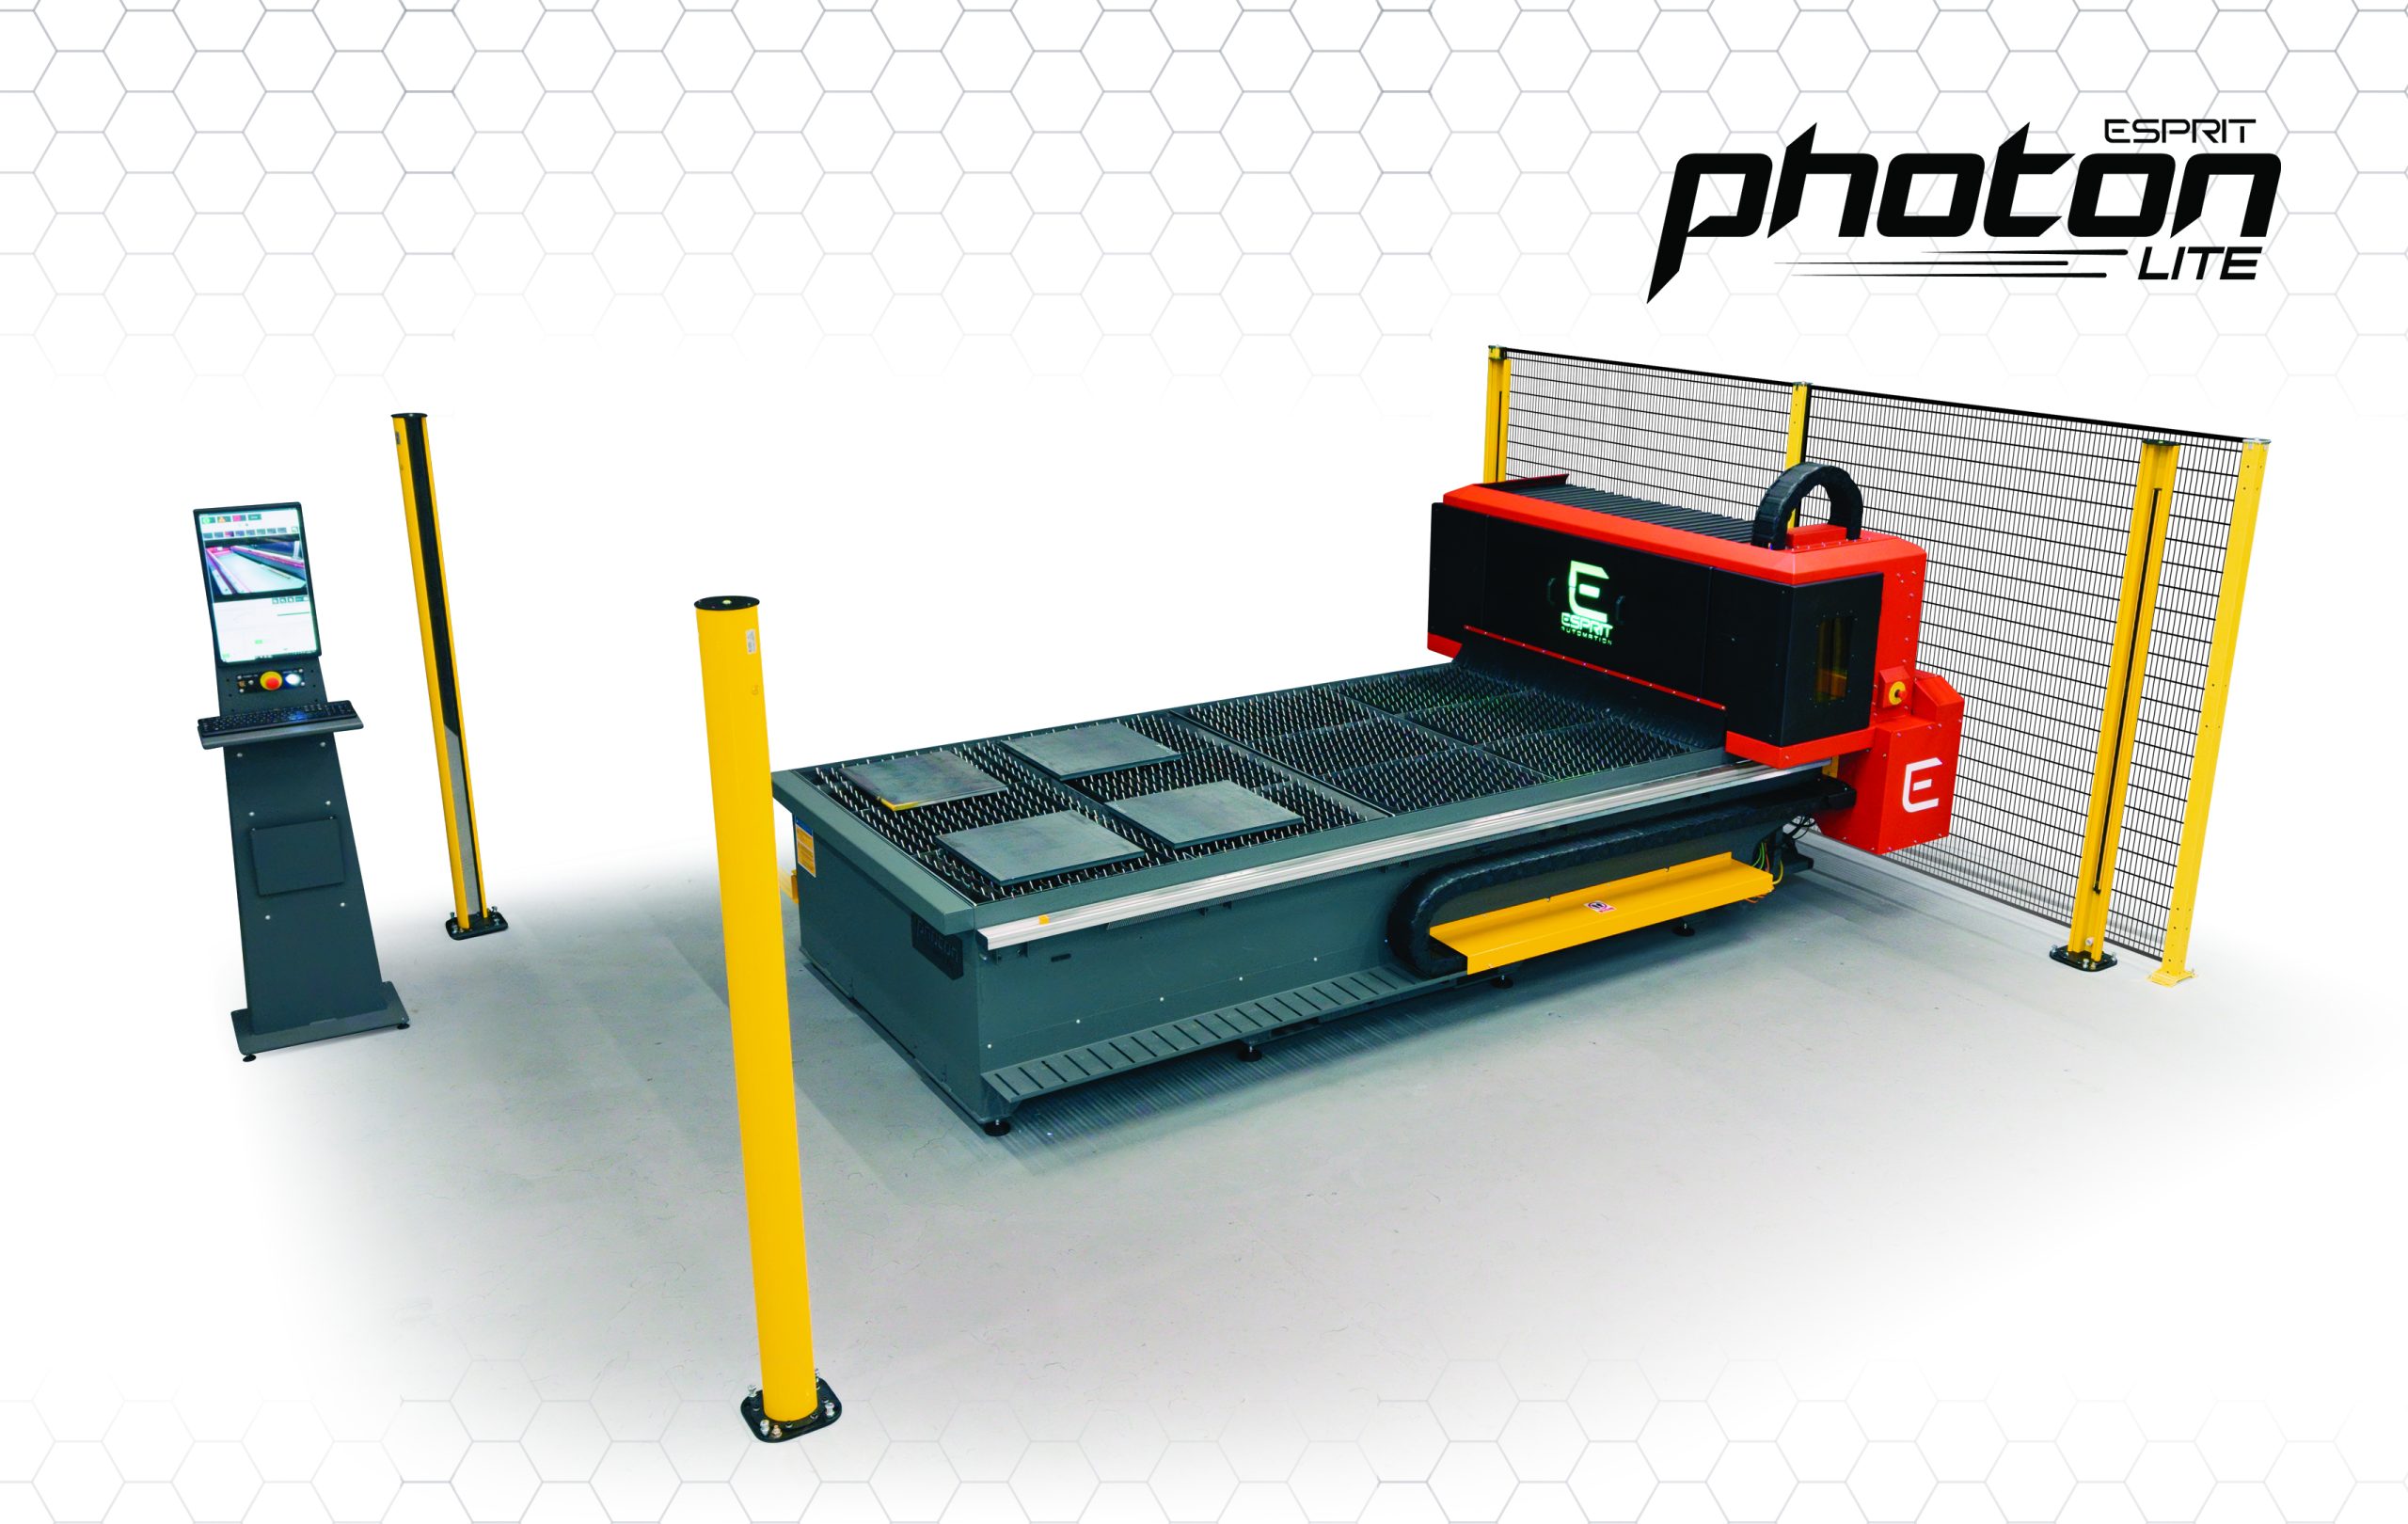
Photon LITE CNC fiber laser cutter manufactured in Nottingham UK by Esprit Automation Featured Laser

Photon LITE CNC Fiber Laser Cutter

  • Solid-state fiber laser source up to 12kW
  • Ultra-compact enclosed footprint with safety class 1 optical enclosure
  • Precision linear motion system & high-dynamic rack drive
  • Sub-millimeter kerf width on stainless steel, carbon steel & yellow metals

Engineered in Nottingham to provide growing fabrication workshops with high-precision fiber laser cutting capacity without massive factory floor space or complex power requirements.
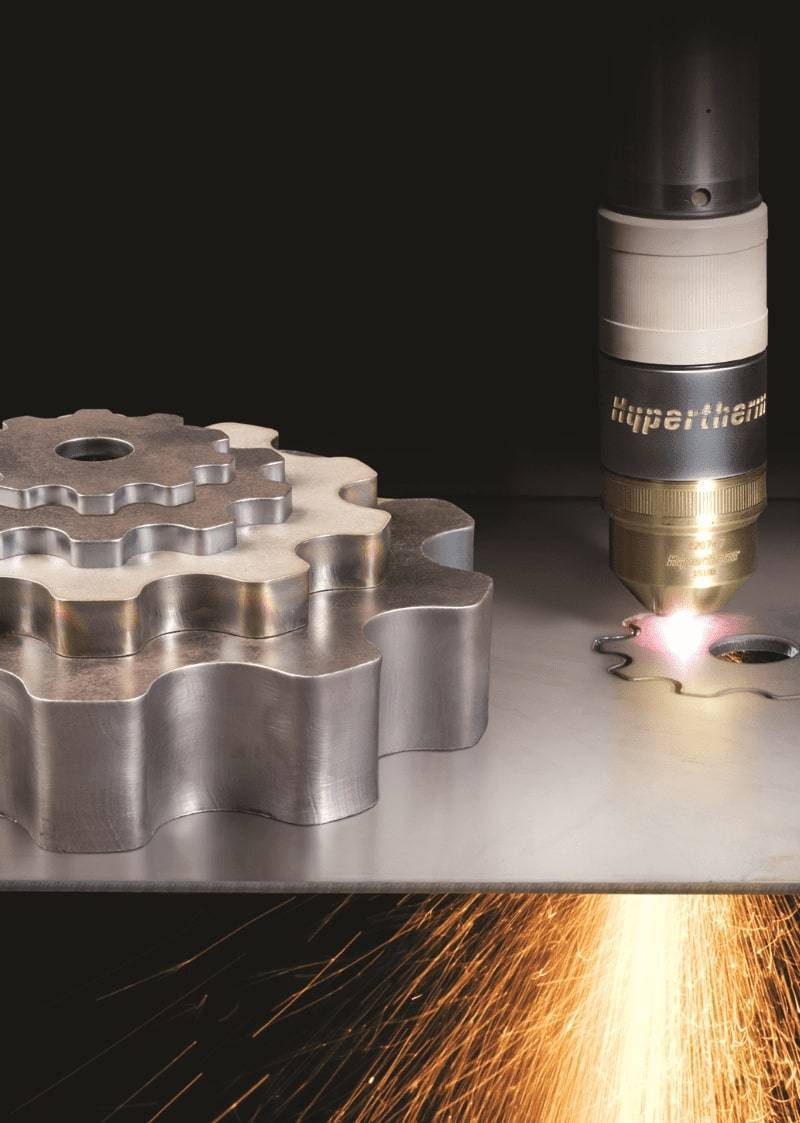
High Definition Heavy Duty Plasma Cutting Table by Esprit Automation High-Volume Heavy Plate

Lightning HD & Viper Heavy-Duty Gantry

  • Hypertherm XPR high-definition plasma power integration
  • Heavy-section machined gantry for continuous multi-shift usage
  • Production piercing capacity up to 50 mm plate thickness
  • Ideal complement or alternative for thick plate steel processing

For fabricators processing structural steel, heavy machinery parts, or rusted/scaled plate above 20 mm where fiber laser assist gas costs rise sharply compared to HD plasma power sources.

Multi-torch CNC oxyfuel flame cutting machine for thick carbon steel Thick Plate Heavy Industry

Heavy-Duty Rail-Based Flame Cutters

  • Multi-head oxyfuel torch configurations (up to 300 mm carbon steel)
  • Custom bed lengths and heavy structural bed frames
  • Can be combined on hybrid gantries with plasma or laser marking heads
  • Lowest consumable cost per meter on carbon steel plate over 50 mm

Designed for heavy engineering facilities, shipyards, and steel stockists requiring simultaneous cutting of identical thick steel profiles with absolute structural reliability.

Engineering Data Matrix

Technical Comparison: Fiber Laser vs High-Definition Plasma vs Oxyfuel Flame


Selecting the ideal CNC thermal cutting technology requires evaluating edge perpendicularity, heat-affected zones (HAZ), operational speeds, and running cost profiles across material ranges.

Comprehensive Thermal Cutting Technology Matrix (ISO 9013 Standards)
Parameters & Metrics CNC Fiber Laser Cutter High-Definition Plasma (XPR) Oxyfuel Flame Cutter
Optimal Thickness Range 0.5 mm – 25 mm (Thin sheet to medium plate) 3.0 mm – 50 mm (Medium to thick plate) 25 mm – 300+ mm (Heavy industrial carbon steel)
ISO 9013 Edge Perpendicularity Range 1 to Range 3 (Near-zero taper, ultra-tight) Range 2 to Range 4 (Excellent angularity) Range 3 to Range 5 (Square top, slight undercut)
Kerf Width (Beam / Arc Slot) 0.08 mm – 0.4 mm (Minimal material waste) 1.2 mm – 3.8 mm (Standard nesting clearance) 2.5 mm – 6.0 mm (Wider allowance required)
Heat-Affected Zone (HAZ) Extremely Low (Preserves metallurgical grain structure) Moderate (Requires minimal post-edge preparation) High (Pronounced heat transfer into thick plate)
Energy Wall-Plug Efficiency ~35% – 45% (Solid-state laser diodes) ~15% – 25% (Arc discharge power supplies) N/A (Exothermic chemical combustion)
Non-Ferrous Processing Outstanding (Aluminium, Brass, Copper, Stainless) Very Good (With specialized gas mixes / H35) Not Capable (Ferrous carbon steel only)
Primary Cost Drivers Laser assist gas (N₂/O₂) & initial optics CapEx Electricity, plasma gas, electrodes/nozzles Fuel gas (Acetylene/Propane) & Oxygen supply
Deep Financial & Technical Analysis

CNC Fiber Laser Cutter Power Selection & Assist Gas Operating Economics


When global procurement teams evaluate a CNC Fiber Laser Cutter, selecting the appropriate laser power (kW) and assist gas configuration directly governs hourly operational expenses and output speed. Solid-state fiber lasers utilize an Ytterbium-doped optical fiber core, operating at a wavelength of approximately 1.07 microns—yielding 10 times higher absorption in metals compared to legacy CO₂ lasers.

1. Laser Power kW Selection vs Material Yield

  • 3kW – 4kW Fiber Laser: Optimal for high-speed sheet metal fabrication (0.5 mm to 6 mm stainless steel and carbon steel). Achieves maximum feed rates on thin gauge components with lower power system infrastructure.
  • 6kW – 8kW Fiber Laser: The versatile sweet spot for general precision engineering. Pierces and cuts up to 15 mm stainless steel with high-pressure Nitrogen and up to 20 mm mild steel with Oxygen assist gas.
  • 12kW – 20kW+ High-Power Fiber Laser: Engineered for heavy structural fabricators. Enables high-speed Nitrogen "burst cutting" on thick gauge stainless and carbon steel, eliminating oxide layer formation for immediate weld-readiness.

2. Assist Gas Cost Breakdown (Nitrogen vs Oxygen vs High-Pressure Air)

Assist gas represents up to 60% of hourly running costs on a CNC fiber laser cutting machine. Choosing the right assist gas strategy significantly affects total cost per part:

  • Nitrogen (N₂) Cutting: High-pressure displacement process (14–25 bar) that blows molten metal out of the kerf without chemical reaction. Produces bright, oxide-free edges ready for immediate powder coating or welding without manual grinding. Higher gas volume cost, but saves secondary labor.
  • Oxygen (O₂) Cutting: Exothermic reaction process operating at low pressure (0.5–3 bar). Oxygen reacts with carbon steel to add thermal energy, reducing electrical power requirements for thick steel cutting. Leaves a thin oxide scale on the cut edge that may require removal prior to painting.
  • High-Pressure Compressed Air Cutting: Filtered, oil-free dried air (78% N₂) compressed to 16–20 bar offers a highly economical alternative for mild steel and stainless up to 10 mm, reducing gas expenses by up to 75% compared to delivered liquid Nitrogen.
Esprit Automation precise engineering and component integration Esprit UK Manufacturer since 1986
35+ Years of British Engineering Heritage

Why Global Specifiers Partner with Esprit Automation


Founded in 1986 by two visionary engineering graduates from the University of Nottingham, Esprit Automation has manufactured heavy-duty, high-precision CNC cutting machines continuously for nearly four decades. Unlike brand marketers who outsource machine manufacturing to low-cost overseas assembly plants, Esprit engineers control every stage of production under one roof in Sandiacre, Nottingham.

Our commitment to technical excellence and client accountability is built into our core operations:

In-House Machine Tool Fabrication

Every bed frame and gantry is stress-relieved, precision machined on large-bed CNC centers, and hand-fitted in Nottingham.

World-Class Tier-1 Components

We integrate premium optics, high-performance laser sources, linear drives, and Hypertherm power systems for max uptime.

Direct Field Service Engineers

Speak directly to the electrical and mechanical technicians who built your machine. Remote controller diagnostic capabilities worldwide.

Guaranteed Spares Availability

We maintain comprehensive UK spares inventory for legacy machines, keeping systems operational across decades of service.

Machining heavy CNC gantry in Nottingham factory Precision welding of machine frames by Esprit engineers In-house CAM software development team Final quality sign-off and electrical testing in Nottingham
Frequently Asked Questions

Global Procurement FAQ: CNC Fiber Laser Cutters & Thermal Cutting Systems


Engineered answers to common AI-driven queries and buyer concerns regarding machine specification, maintenance, safety compliance, and total financial return.

The primary deciding factors are material thickness, required edge tolerance, hole diameter ratios, and production volume. CNC Fiber Laser Cutters excel on sheet metal and light-to-medium plate up to 20–25 mm, delivering sub-millimeter tolerances, tight kerf widths, minimal heat affected zones (HAZ), and unmatched speed on thin gauge stock. High-Definition Plasma (such as the Hypertherm XPR family) remains the most cost-effective capital choice for medium-to-thick plate from 6 mm to 50 mm, particularly on mild steel with mill scale, paint, or rust where laser optics would require frequent cleaning or high assist gas costs.

Assist gas selection directly affects operational overhead. High-pressure Nitrogen (14–25 bar) consumes significant gas volume, producing an oxide-free, weld-ready edge on stainless steel and aluminium. Oxygen assist gas (0.5–3 bar) lowers gas consumption costs on thick carbon steel via exothermic combustion, but leaves a thin oxide layer. Utilizing high-pressure compressed air (16–20 bar) with specialized multi-stage oil and water filtration systems provides a highly economical middle-ground for mild steel and stainless up to 10 mm, reducing assist gas expenses by up to 75% compared to liquid Nitrogen.

Modern solid-state fiber laser sources feature mean time between failures (MTBF) exceeding 100,000 operational hours for optical laser diodes. Routine maintenance focuses on consumable components within the cutting head: protective cover glass inspection/replacement, nozzle centring, ceramic ring checks, and dust filtration filter element rotation. Keeping the optical path completely sealed and maintaining ambient temperature/humidity control via an integrated chiller unit ensures consistent beam performance across years of continuous operation.

Fiber laser cutting operates at a 1.07-micron wavelength, which presents a significant retinal safety hazard. Consequently, industrial laser cutting machines must be fully enclosed in Class 1 optical safety housings with certified laser safety glass viewing windows. Furthermore, high-velocity laser cutting produces fine respirable metal particles. Compliant installations require downdraught extraction tables with automatic pneumatic zone switching, coupled with explosive-dust certified (ATEX compliant) industrial fume filtration units using nanofiber cartridge filters to conform to UK HSE COSHH and European CE/UKCA regulations.

Yes. Esprit CNC cutting systems utilize open-architecture control technology compatible with industry-standard CAD/CAM nesting software packages such as Hypertherm ProNest, Lantek Expert, SigmaNEST, and MetaCAM. Our controllers accept standard DXF, DWG, and NC code files. They support direct automated network transfer, remote job scheduling, real-time machine telemetry feedback, and OPC-UA connectivity for integration into modern Industry 4.0 smart factory environments.

Esprit cutting machines operate in more than thirty countries worldwide. International customers are supported directly by our Nottingham engineering team via secure remote network controller diagnostics, allowing our software specialists to troubleshoot parameters instantly. For on-site service, routine calibration, or emergency mechanical repairs, we deploy factory-trained regional field service engineers backed by express international dispatch of genuine OEM spare parts and consumables from our central inventory.

Direct Factory Engineering Consultation

Request Your Customized CNC Fiber Laser Cutter Proposal


Whether you need to cut precise thin stainless components, heavy carbon steel plate, or expand your factory's production capacity, our engineering team in Nottingham is ready to assist. Send us your CAD drawings or part schedules for a complimentary cut time calculation, assist gas cost model, and formal quotation.

Esprit Automation Ltd stacked logo
Direct Telephone
+44 (0)115 939 1888
Engineering Email
[email protected]
Nottingham Headquarters
Esprit Automation Ltd
Plackett Mill, Church Drive
Sandiacre, Nottingham, NG10 5EE
United Kingdom
Business Hours
Monday – Friday, 08:30 – 17:00 (GMT)