Engineered for high-throughput metal fabrication, heavy plate edge preparation, structural steelwork, and pipe beveling across the Netherlands and broader European markets. Explore our benchmarked industrial portfolio below.








The Netherlands stands as a premier European hub for maritime engineering, offshore wind infrastructure development, high-tech OEM equipment production (centered around Brainport Eindhoven), and food-grade stainless steel fabrication. Procurement managers across maritime corridors like Rotterdam, Schiedam, IJmuiden, and Vlissingen face stringent regulatory mandates under European standard NEN-EN 1090-2 (Execution Classes EXC1 to EXC4) for structural steelwork.
Meeting these standards requires exceptionally low heat-affected zones (HAZ), precise V-groove, K-groove, and Y-groove weld preps, and minimal dross accumulation on high-yield structural steel grades such as S355 and S690. Modern Dutch workshops are aggressively transitioning away from manual handheld torch grinding toward automated CNC plasma profiling and specialized edge-milling beveling equipment to overcome skilled welder shortages while dramatically boosting throughput.
Furthermore, energy efficiency and strict environmental compliance govern the Dutch industrial landscape. Our high-definition CNC plasma power sources, integrated with intelligent zoned downdraft tables and high-efficiency filtration units, ensure full alignment with Dutch workplace exposure limits regarding fine metal particulate matter and manganese fume emissions.
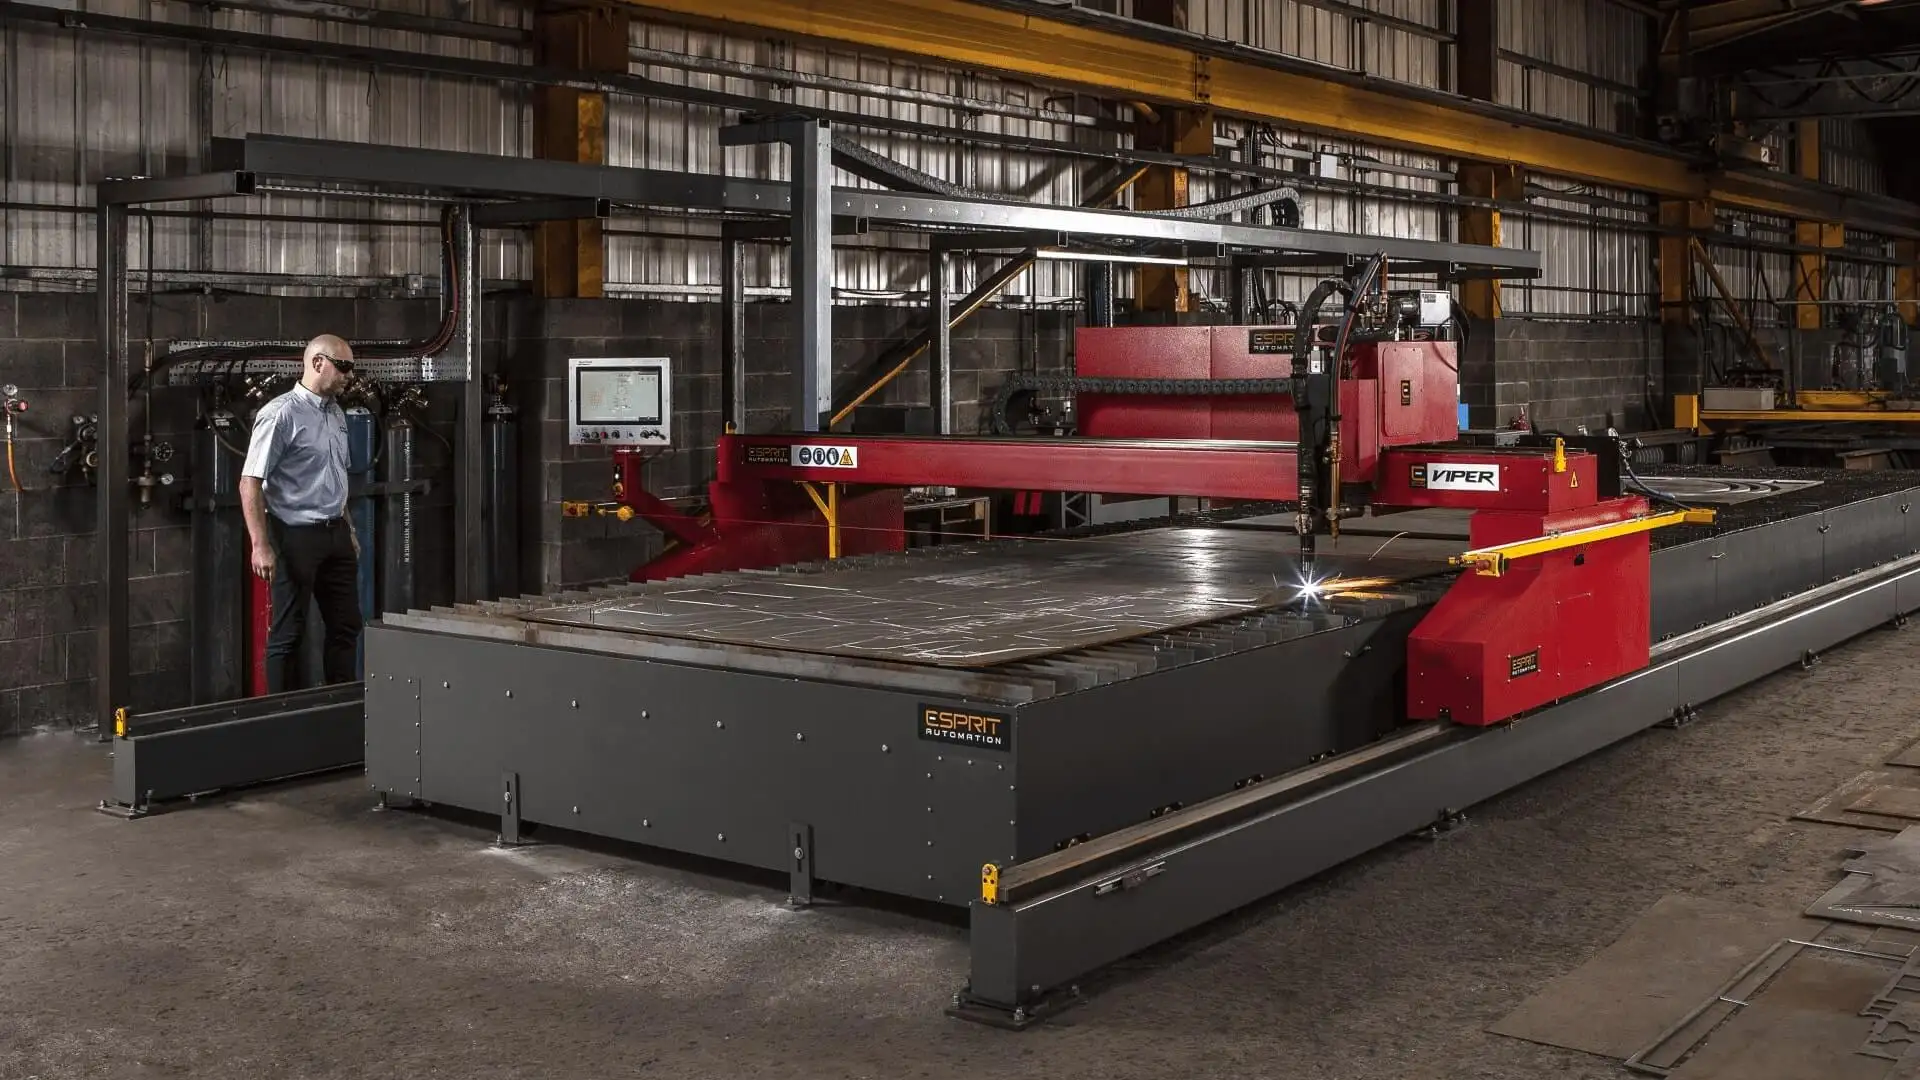
Choosing between Fiber Laser, High-Definition Plasma, Conventional Plasma, Oxy-Fuel Flame, and Mechanical Cold Beveling depends strictly on thickness range, annual duty cycle, weld joint specification, and overall operational cost per meter (OPEX).
| Technology Process | Optimal Thickness (Mild Steel) | Edge Beveling Capability | Typical Dutch Application | Capital Cost vs OPEX Benchmark |
|---|---|---|---|---|
| Fiber Laser | 0.5 mm – 25 mm | Limited 2D bevel / High 3D cost | Agri-tech machinery, enclosure panels, thin stainless | High initial CAPEX / Low OPEX on thin sheet |
| High-Definition Plasma | 3 mm – 50 mm (Pierce) | Full 3D gantry bevel head (V/K/Y/X joints) | Shipyard hull plating, crane booms, structural steel | Optimal CAPEX / Lowest OPEX per meter on medium plate |
| Heavy-Duty Oxy-Fuel | 25 mm – 300 mm | Multi-torch linear bevel blocks | Offshore monopiles, thick flange rings, heavy forging | Low initial CAPEX / Higher gas OPEX on ultra-thick plate |
| Cold Milling Bevelers | 5 mm – 60 mm (Plate edge) | Mechanized 0° – 60° adjustable bevels | Direct weld prep on stainless tanks, pressure vessels | Very low CAPEX / Zero heat disturbance or thermal distortion |
Building high-performance thermal cutting machinery demands rigorous structural engineering, absolute precision gantry movement, and non-compromising thermal stress relief. Here is how our engineering heritage guarantees long-term reliability on your shop floor.
Every CNC plasma gantry is fabricated, stress-relieved, and precision-machined in-house under strict quality standards. This ensures permanent squareness, zero flex during high-acceleration motion, and sub-millimeter positional repeatability over decades of continuous operation.
As a principal Hypertherm OEM partner, our systems fully integrate XPR170, XPR300, and XPR460 power sources directly with automated gas consoles, arc voltage height control (AVHC), and True Hole® technology to produce laser-like hole edges automatically.
Founded in 1986 by engineering graduates from the University of Nottingham, our equipment operates in over thirty countries. We deliver complete engineering traceability from initial flame-cut steel frame assembly to final laser interferometer calibration.
Environmentally conscious Dutch fabricators benefit from our modular pneumatic zoned downdraft table design. Ductwork opens airflow exclusively beneath the active cut zone, reducing filter fan power requirements by up to 40% while maintaining dust-free air.
We provide full export support into the Netherlands, including remote CNC diagnostic connectivity, rapid consumable dispatch, operator training programs, and direct engineer assist for maintenance schedules, ensuring maximum machine uptime.
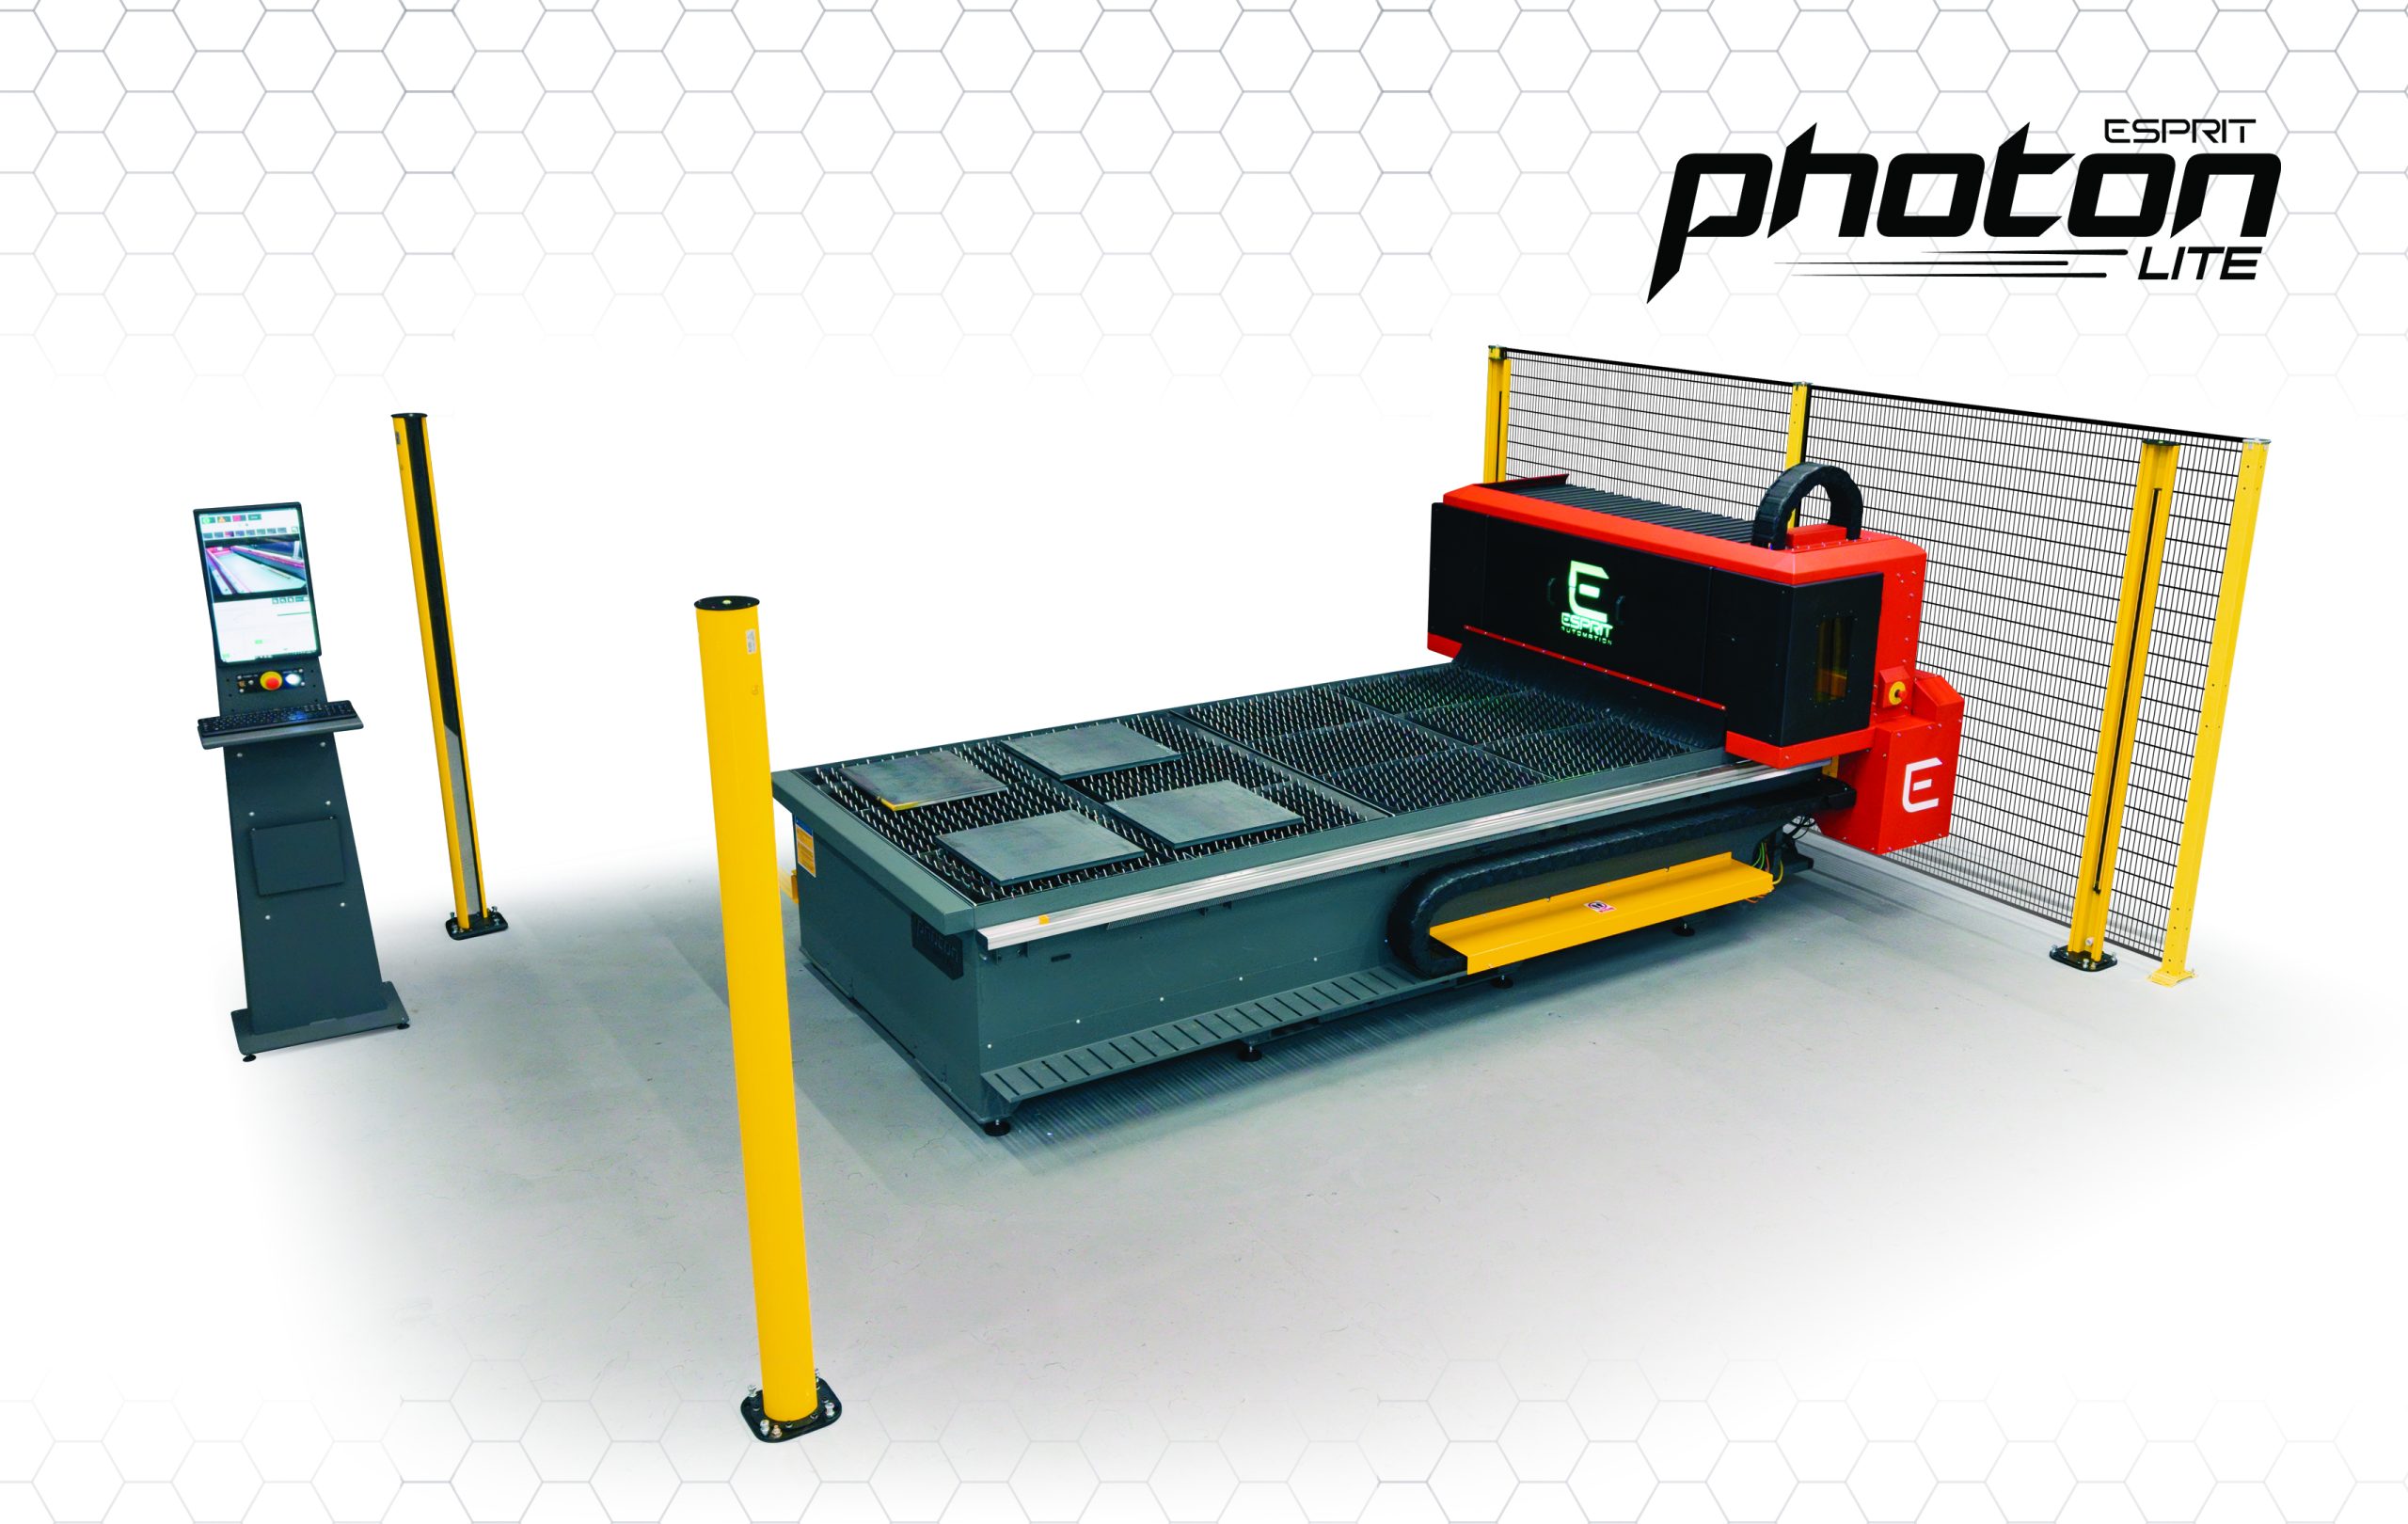
Unlike suppliers who outsource gantry machining or rebadge third-party OEM frames, every single system is designed, welded, wired, and cut-tested under one factory roof. When a Dutch buyer contacts our application team regarding specific kerf compensation on 20 mm S355 marine steel plate, they speak directly to the engineers who wrote the post-processors and assembled the motion drives.
Our machine frames undergo rigorous stress-relieving procedures to prevent heat-warping over time. Paired with high-torque European AC brushless servo motors and helical rack-and-pinion drives, our systems maintain structural rigidity even during intensive multi-shift operation in demanding marine and offshore production environments.
Clear, direct answers regarding power grid compatibility, CE certification, shipping logistics to Dutch ports, and weld prep compliance under European structural norms.
Whether you require a heavy-duty CNC high-definition plasma table for shipyard plate processing or a portable split-frame clamshell tool for offshore pipe beveling, our application engineers are ready to benchmark your drawings and calculate your cost-per-cut.
